Seamless activewear represents the pinnacle of modern functional performance apparel. By utilizing cutting-edge Santoni circular tubular knitting technology, our integrated facility in Sialkot, Pakistan eliminates traditional side seams, minimizes friction points, and integrates micro-zoned muscle stabilization directly into the fabric matrix. As an audited OEM and ODM production powerhouse, we provide end-to-end technical garment development, multi-stage fabric verification, bespoke private label packaging, and export logistics tailored for North American, European, Australian, and Middle Eastern distribution channels.
Examine our precision-crafted production archetypes. Each product is customizable in fabric blend (Polyamide 6.6, Recycled Poly, Elastane), GSM weight, compression profiling, Pantone shade matching, and custom branding.
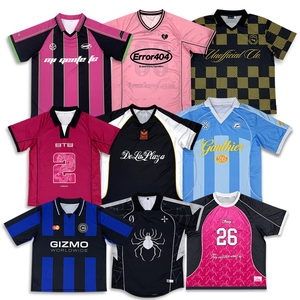
Engineered micro-interlock polyester with high-definition digital dye sublimation. Oversized modern streetwear cut with reinforced anti-stretch neck ribbing.
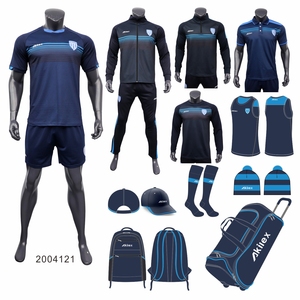
High-ventilation jacquard mesh panels mapped to perspiration zones. Quick-dry filament yarn ensuring colorfastness under intense match conditions.
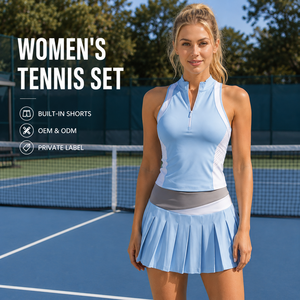
UV-blocking nylon-elastane fabric with 4-way mechanical stretch. Integrated inner compressive undershort with non-chafing ball pockets.
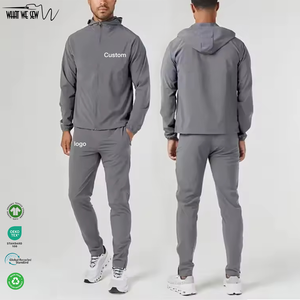
DWR-coated ripstop membrane with internal mesh lining. Waterproof seam-sealed reverse coil zippers and wind-resistant anatomical hood structure.
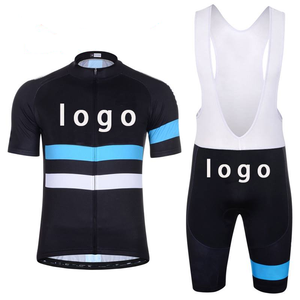
Aerodynamic channel fabric construction on shoulders and sleeves. Triple reinforced back utility pockets with integrated 3M reflective safety detailing.
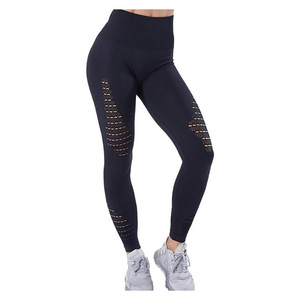
Santoni 28-gauge tubular knit using air-jet texturized polyamide and covered spandex. Zero front rise seam, double-layer compressive tummy-tuck waistband.
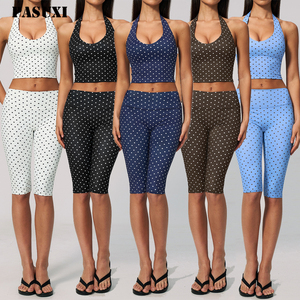
Micro-ribbed underbust stabilization band, removable breathable molded cups, and contoured glute-enhancing shading knit directly into the seamless structure.
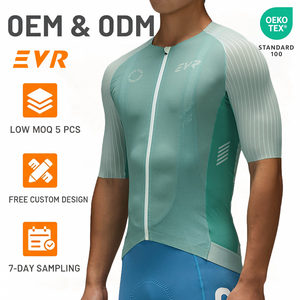
Low-drag textured warp knit engineered for pro racing peloton dynamics. Silicone waist hem grippers and anti-bacterial UPF 50+ surface finishing.
Traditional athletic wear manufacturing relies heavily on cut-and-sew operations, in which 2D fabric panels are cut from rolled bolts and assembled along stitched seams. This outdated assembly method introduces elevated friction zones, prone-to-failure thread seams, and up to 22% scrap fabric waste during pattern grading. In contrast, our advanced seamless activewear manufacturing leverages computerized Santoni circular knitting machinery to create tubular 3D garments directly from yarn packages.
Through electronic needle-by-needle needle selection, we engineer dynamic compression gradients, open-knit ventilation mesh, and rib-reinforced core stabilization zones simultaneously within a single continuous tubular weave. This eliminates side seams completely, enhancing mechanical durability during 100% elongation stress tests and reducing overall garment assembly lead times.
By modulating feed yarn tension across circular rows, we integrate firm muscular compression over hamstrings and quadriceps while relaxing density over joint articulation points for unrestricted movement.
We combine Polyamide 6.6 with covered Spandex (Elastane) using air-jet texturing, preventing the common "sheen" of cheap polyester and providing a luxurious, buttery, squat-proof matte finish.
Circular knitting knits garments to precise body diameter cylinders. This reduces cutting room textile scrap by over 80% compared to conventional cut-and-sew operations, boosting sustainability compliance.
Navigating the global sportswear market requires anticipation of technological, ecological, and supply chain shifts. Brand managers and global buyers must balance sustainability legislation with high-performance consumer demands.
Global regulatory bodies like the EU Textile Strategy are mandating measurable post-consumer recycled content. The future belongs to chemically recycled Polyamide (rPA6) and bio-based nylon derived from renewable castor beans, offering the exact same tensile resilience and color uptake as virgin polymers while eliminating virgin fossil fuel dependency.
Protracted lead times from East Asian monolithic production centers have forced western brands to diversify toward flexible industrial hubs like Pakistan. Sialkot's integrated supply clusters allow raw yarn spinning, specialized knitting, laboratory testing, and international air/sea freight dispatch to occur within a 25-kilometer radius, slashing sample-to-market cycles by up to 35%.
Consumer expectations have transitioned from purely aesthetic gym wear to biomechanically functional gear. Brands are demanding clinical-grade graduated compression (15-20 mmHg) that promotes venous blood return, reduces delayed onset muscle soreness (DOMS), and utilizes hollow-core thermal filament yarns for year-round temperature autoregulation.
Direct comparisons between commercial grade performance fibers, knitting machine gauge configurations, and recommended applications for OEM/ODM private label program procurement.
| Yarn Composition | Knitting Gauge | GSM Range | Target Application | Key Technical Benefit |
|---|---|---|---|---|
| Polyamide 6.6 (Nylon) + Elastane (85/15) | 28-Gauge Santoni Circular | 260 - 320 GSM | Squat-Proof Leggings & Gym Sets | Exceptional surface abrasion resistance, zero pilling, ultra-soft matte handfeel |
| Recycled Micro-Polyester + Spandex (88/12) | 24-Gauge Circular Knit | 180 - 240 GSM | Running Tops & Team Uniforms | Rapid moisture transport, high tensile resistance to full-dye sublimation heat |
| Cationic Poly + Nylon + Spandex (50/40/10) | 28-Gauge Dual Feeder | 240 - 290 GSM | Marl / Heather Athleisure Sets | Dual-tone yarn piece-dyeing capability, high visual texture without print cracking |
| Polypropylene (Dryarn) + Polyamide (60/40) | 32-Gauge High-Density | 140 - 190 GSM | Pro Cycling Base Layers & Skiwear | Lowest thermal conductivity of any fiber, hydro-phobic vapor expulsion |
Why tier-one sportswear brands, professional soccer clubs, and fast-scaling fitness startups partner directly with our Sialkot manufacturing facilities for their private label programs.
Work directly with our pattern designers, textile technicians, and production directors. Transparent FCL/LCL commercial pricing without trading company markups or lost communication nuances.
Don't have an engineering tech pack? Our in-house design unit transforms your physical samples, CAD sketches, or digital concept boards into industrial grading charts (XS through 5XL plus youth sizes).
From initial raw yarn elongation verification to inline stitch audits, 10-wash cycle stress tests, and final carton pre-shipment inspections, our QA safeguards your brand equity at every turn.
Complete private label execution: heat-transfer seamless neck prints, silicone branding badges, recycled biodegradable frosted polybags, retail hangtags, and compliant EAN/UPC barcode labeling.
Transparent stage gates ensure zero margin for error between digital tech pack approval and international warehouse delivery.
Yarn denier selection, Pantone color lab-dip matching, stitch density parameter mapping, and commercial costing finalized within 48 to 72 hours.
Knitting the first proto sample, physical fit modeling, stretch recovery testing, and courier dispatch for buyer review in 7 to 14 business days.
Continuous automated knitting, seam joining (flatlock/overlock/merrow), high-temperature boarding, piece dyeing, and daily inline stitch inspections over 3 to 5 weeks.
Colorfastness to laundering (ISO 105-C06), dimensional stability, burst strength testing, and metal detection screening prior to garment folding.
Placement of individual silicone tags, custom printed cardstock hangtags, desiccant pouches, master export carton sealing with reinforced strapping.
Coordinated sea freight (FOB Karachi, CIF destination port) or expedited door-to-door DDP air cargo with complete commercial customs documentation.
Detailed technical, financial, and logistical insights addressing the most critical procurement inquiries submitted by apparel importers, brand founders, and team distributors.
Whether you require precision circular-knit seamless leggings, custom-sublimated football team kits, aerodynamic cycling apparel, or private label gym wear, our engineering team in Sialkot is prepared to evaluate your project specifications and deliver competitive factory-direct quotations.
