Direct-from-factory sportswear manufactured with multi-filament polyester, high-tenacity nylon-spandex blends, and micro-porous breathable interlocks. Each blank is calibrated for private label relabeling, DTF, embroidery, screen printing, or full all-over dye sublimation.
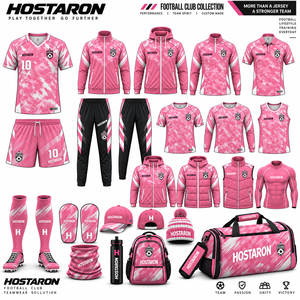
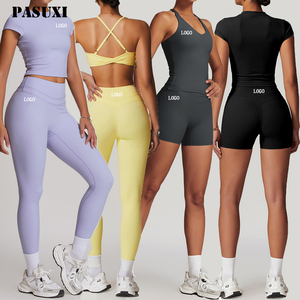
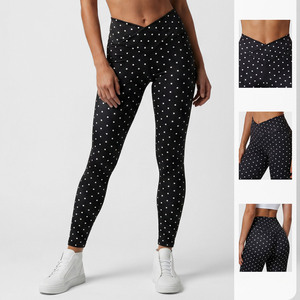
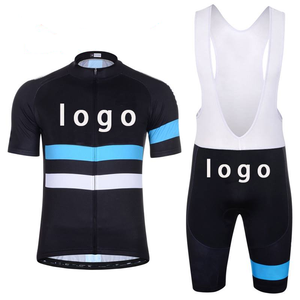
How leading performance activewear brands, sportswear distributors, and DTC fitness labels are balancing technical yarn engineering, tariff mitigation, and ultra-flexible supply chain architectures.
The international sourcing paradigm for athletic wear, functional training apparel, and team sportswear has crossed an irreversible threshold. Global brand directors, corporate merchandise buyers, and performance startup founders are no longer seeking generic commodity apparel factories. In modern competitive landscapes, commercial success hinges upon partnering with an agile, vertically integrated Custom OEM Blank Athletic Apparel Manufacturer & Exporter capable of delivering precise fiber mechanical characteristics, certifiable environmental compliance, and compression grade reproducibility.
Historically, commercial blank apparel programs were characterized by thick, tubular cotton knits with standard tubular side construction. Today's commercial athletic market demands hyper-specialized technical blanks engineered from multi-filament micro-denier polyamides, recycled post-consumer PET bottles (rPET), and polyether-polyurea copolymer (spandex/elastane) matrices. These textiles must achieve specific thermodynamic equilibrium: managing convective moisture dissipation, offering resistance to hydrolytic degradation from body perspiration, retaining structural elastomeric memory over 100+ industrial wash cycles, and remaining strictly opaque (squat-proof) under high mechanical elongation.
At the center of this industrial evolution is the Sialkot textile cluster in Punjab, Pakistan. Known globally as the premier manufacturing epicentre for sporting goods, football kits, combat fitness wear, and high-performance garments, Sialkot combines generational technical tailoring with high-speed automated digital sublimation machinery, Japanese programmable computerized multi-needle flatlock machines, and integrated laboratory test suites. When international buyers partner with our OEM/ODM facilities, they bypass trading middlemen, eliminate markups of 25%–40%, and achieve direct engineering control over every tech pack parameter—from yarn denier counts to final retail barcode packaging.
Key structural shifts every sports apparel procurement manager, fashion buyer, and teamwear brand director must integrate into their multi-year sourcing roadmaps.
Global brands are mitigating warehousing carry costs by procuring modular "core blanks"—unbranded, precision-patterned base stock garments held in inventory, ready for rapid spot-market customization via high-density silicone transfer, direct-to-film (DTF), or club embroidery within 72-hour fulfillment cycles.
Regulatory mandates such as the EU Corporate Sustainability Due Diligence Directive (CSDDD) are pushing commercial buyers toward Global Recycled Standard (GRS) certified polyester, bio-based nylon polymers, and closed-loop sublimation inks that emit zero toxic volatile organic compounds (VOCs).
Transitioning away from cut-and-sew bulk panels, high-end athletic activewear utilizes computerized Santoni circular jacquard machines. This enables engineered micro-mesh ventilation zones and graduated muscular compression along targeted zones without standard chafing seam margins.
Brands are leveraging 3D CLO and Browzwear CAD assets to finalize virtual garment fit iterations prior to physical sampling. Our engineering team converts 3D GLTF/OBJ formats directly into automatic cutting-marker files, slashing prototyping lead time down to 7 business days.
Detailed mechanical comparison of industrial fabrics engineered within our knitting and dyeing facilities for wholesale procurement and OEM custom branding.
| Apparel Category | Fabric Composition | Areal Density (GSM) | Tensile / Seam Standard | Primary Functional Mechanism | Optimal Decoration Process |
|---|---|---|---|---|---|
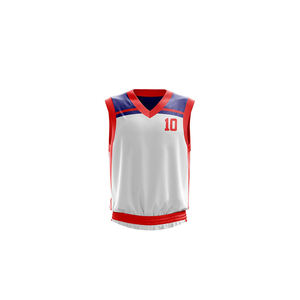
| Teamwear Jerseys (Soccer, Basketball) | 100% Micro-Interlock Poly / Jacquard Mesh | 140 – 160 GSM | ISO 13934-1 ≥ 420N | Capillary wicking cross-section, zero liquid retention | Full Dye Sublimation (210°C) |
| Compression Base Layer (MMA, Running) | 85% Polyester / 15% Spandex (4-Way Stretch) | 200 – 230 GSM | ISO 13936-2 (No Seam Slippage) | Graduated muscular stabilization, lactic acid mitigation | Silicone High-Build / Sublimation |
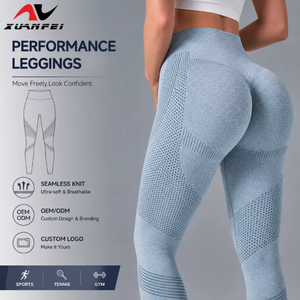
| Sculpting Yoga Leggings (Athleisure) | 75% Polyamide (Nylon 6.6) / 25% Lycra | 250 – 290 GSM | 4-Needle 6-Thread Flatlock | Zero-sheer squat security, brushed peach butter-soft feel | Heat Transfer Film / DTF / Minimalist Tab |
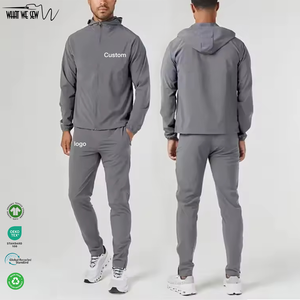
| Pro Team Outerwear (Windbreaker, Warmup) | 100% 70D/90D Taslan / Mechanical Stretch | 110 – 140 GSM | Hydrostatic Head ≥ 3000mm | DWR water-repellency, windbreaker membrane barrier | Direct Embroidery / High-Frequency Patch |
| Gym & Street Fleece (Heavyweight Hoodies) | 80% Combed Ring-Spun Cotton / 20% Poly | 360 – 440 GSM | Pre-Shrunk ≤ 3% Residual | Brushed interior thermal fleece, anti-pilling compact yarn | Screen Print / Puff 3D Print / Appliqué |
From raw filament selection to container drayage, our vertically integrated plant operations in Sialkot, Pakistan, provide an uncompromised competitive moat for global sports apparel brands.
Utilizing computerized Gerber and Optitex pattern grading systems, we achieve nest markers with fabric yield efficiencies exceeding 92.5%. This reduces yardage waste, accelerates material economy, and guarantees precise dimensional balance across North American (US) and European (EU) sizing charts from Youth YS up to Adult 5XL.
Equipped with Italian Kiian and Swiss sublimation inks alongside spectrophotometer testing suites, our digital color laboratories reproduce specific Pantone hues with Delta E (ΔE) color variances maintained below 0.8. Club identities, corporate sponsor logos, and neon seasonal palettes maintain absolute batch-to-batch consistency across subsequent bulk reorders.
High-stress athletic movements require specialized joinery. Our stitching floors house specialized Yamato and Juki industrial machinery configured for ISO 406 (3-thread coverstitch) and ISO 607 (4-needle 6-thread flatlock). By eliminating raised inner seams, our garments deliver second-skin anti-chafing comfort suited for long-distance marathoners, cyclists, and elite contact athletes.
Our Quality Assurance team acts as an independent inspection bureau inside the plant. Quality gates are active across 4 nodes: Greige Fabric Inward Audits (4-point system), Pre-Cutting Shrinkage Relaxing (24 hours minimum), Inline Stitched Seam Tensile Verification, and Final Inspection conforming to Military Standard 105E (MIL-STD-105E) / ISO 2859-1 AQL 2.5 Major / 4.0 Minor.
Operating as a registered exporter in Pakistan, we generate verified Certificates of Origin (COO), GSP preferential customs documentation, detailed packing lists with volumetric weight calculations, and carton barcoding. Whether shipping via air express (DHL/FedEx) or sea consolidation via Karachi port, our shipments clear customs smoothly in North America, the UK, Europe, Australia, and the GCC.
Clear, uncompromising answers to help sourcing directors, brand managers, and apparel importers plan their custom OEM blank manufacturing programs.
Our MOQ is designed to support both agile brand rollouts and mass retail orders. For fully sublimated blank jerseys and custom sportswear, our MOQ starts at 30 to 50 pieces per design across assorted sizing (S–3XL), since digital sublimation transfers do not require screen tooling. For custom-dyed solid knit activewear (such as custom nylon-spandex yoga leggings or peached French terry fleece), the standard MOQ is 200 to 300 pieces per colorway, which matches the minimum volume of our pressurized laboratory dyeing vats.
We work seamlessly with both complete PDF tech packs and initial physical benchmark samples. If you have an established specification sheet, our CAD pattern masters import your graded points directly. If you only possess a physical sample or conceptual reference garment, our ODM engineering unit reverse-engineers the piece, builds the technical spec sheet, digitizes the graded sizing curve (XS–5XL), and issues 3D virtual renderings for your structural sign-off prior to cutting physical fabric.
Rapid speed-to-market is central to our facility operations. Prototype development and strike-off lab dips typically require 7 to 12 business days depending on fabric availability and trim customization. Once your "Golden Pre-Production (PP) Sample" receives final sign-off, commercial bulk manufacturing generally takes 3 to 5 weeks. Urgent club season orders can access our rapid-turnaround production lines upon request.
Yes. We operate complete private label finishing lines. Options include woven damask neck labels, heat-transfer satin wash tags, branded paper swing tags with UV spot printing, QR code/UPC barcode adhesive stickers, individual biodegradable or zip-lock frosted EVA polybags, and heavy-duty 5-ply export master cartons strapped for ocean freight or Amazon FBA / 3PL warehouse intake.
All bulk fabric rolls undergo standardized in-house physical lab tests: dimensional stability after washing (AATCC 135 / ISO 6330) with guaranteed shrinkage kept under 3%–4%; colorfastness to washing and perspiration (ISO 105-C06 / E04) achieving Grade 4.0 or above; and Martindale abrasion resistance testing to prevent pilling and premature fabric breakdown under intense athletic abrasion.
We work routinely under standard international commercial terms, including FOB (Karachi), CIF, and full DDP (Delivered Duty Paid) where we manage ocean/air transit, import customs clearance, and road carriage directly to your local logistics hub. Commercial transactions are handled securely via Wire Transfer (T/T with initial deposit and balance upon Bill of Lading copy) or Irrevocable Letters of Credit (L/C at sight) for multi-container institutional contracts.
Eliminate trading middlemen, gain direct access to Sialkot's technical textile cluster, and access verified production schedules. Speak with our Senior Sportswear Merchandising Engineers today to evaluate tech packs, request laboratory swatch books, or order your pre-production golden samples.
