Explore our flagship OEM/ODM production references. Each design integrates 4-way stretch recovery, squat-tested opacity, and ultra-durable bonded flatlock or seamless circular-knit construction tailored for global distribution.
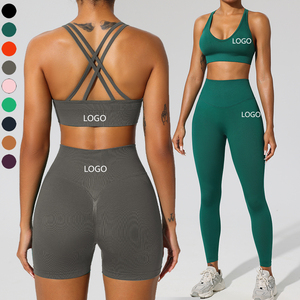
280 GSM ribbed nylon-elastane blend. Features targeted butt-sculpting ruching, core-stabilizing waistband, and moisture-wicking capillary knit.
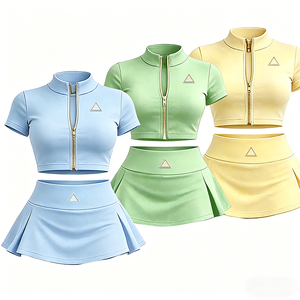
High-density interlock knit with concealed anti-friction bike shorts inside skirt. YKK semi-lock zipper hardware and custom silicone badging.
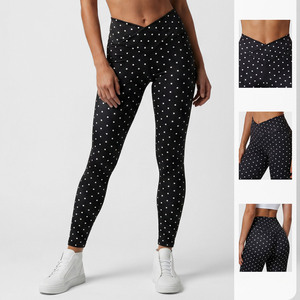
Dual-sided brushed microfilament yarn delivering second-skin weightlessness. Anatomical V-back waistband eliminates gapping during squats.
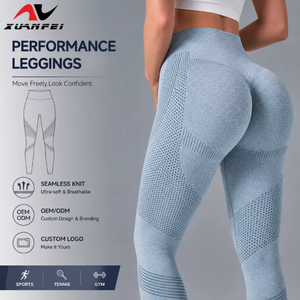
True tubular circular seamless build with graduated abdominal support. Tested to withstand 100+ industrial wash cycles without tensile degradation.
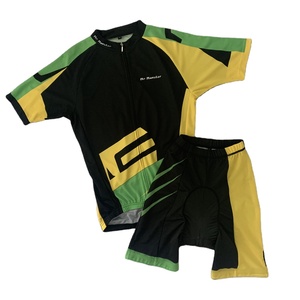
130 GSM aerodynamically channeled honeycomb mesh. Italian non-toxic sublimation inks ensuring razor-sharp graphic acuity and zero skin irritation.
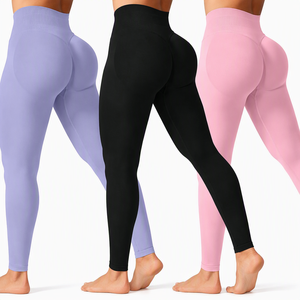
Ultra-clean minimalist profile with blind-stitch hems. Optimized elasticity recovery coefficient prevents post-session knee-sagging.
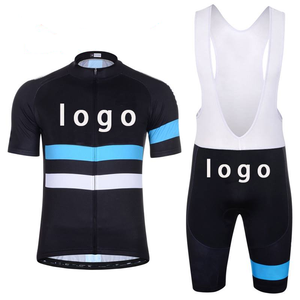
Ergonomic laser-cut silicone gripper cuffs, three rear cargo pockets with reinforced bar-tack stitching, and 360-degree reflective visibility piping.
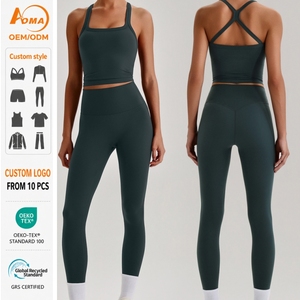
High-support anti-bounce crop top coupled with micro-ruched high-rise tights. Zero underwire pressure with thermal molded compression cups.
The Greater Boston metropolitan area—encompassing Cambridge, the Innovation District, and the Route 128 tech corridor—occupies a singular, revered space in international sports science and athletic apparel architecture. As the historic cradle of competitive distance running, exemplified by the Boston Marathon, and the home base for global footwear powerhouses, pioneering biomechanics institutes, and high-performance collegiate rowing programs along the Charles River, Boston dictates performance trends that ripple across the worldwide sporting goods economy.
However, for forward-thinking brand founders, apparel directors, and private label merchandisers operating in Massachusetts, turning technical prototypes into scalable, commercial-grade seamless workout leggings presents a unique supply-chain friction. While design ateliers and biomaterial labs flourish locally in New England, high-density, multi-axial seamless circular-knitting infrastructure demands capital-intensive machinery, vertically synchronized dye houses, and microscopic tolerances that are predominantly delivered by specialized export manufacturing clusters. Our factory serves as the direct technical bridge: executing OEM and ODM programs with exact Boston-market specifications while maintaining factory-direct pricing, certified ISO 9001 quality controls, and agile supply-chain integration.
Garments built for the Boston market cannot rely on generic, one-dimensional textile formulas. Sourcing managers must cater to an active demographic navigating hyper-variable weather patterns—from freezing, wind-whipped coastal training along Boston Harbor in January to muggy, humid baseline conditioning in July. Seamless knit technology transcends conventional cut-and-sew apparel by varying stitch structure, density, and yarn blend within an unbroken cylindrical tube.
Through Santoni circular-knitting machines, our technical technicians vary tension parameters on the fly. In the quadriceps and hamstring zones, we integrate high-modulus Polyamide 6.6 mixed with dual-core Lycra to stabilize active muscle groups against micro-oscillations that cause fatigue during 20-mile marathon simulations. Concurrently, behind the popliteal fossa (the rear of the knee) and across the lower lumbar region, the machine automatically transitions to an open-structure pique or jacquard ventilation eyelet. This dynamic venting allows rapid evaporative cooling during high-output sessions at indoor boutique studios across Back Bay, Cambridge, and Somerville without requiring a single abrasive thread or seam line.
To successfully capture high-margin retail market share in New England, B2B buyers must align manufacturing tech packs with localized user habits. Our manufacturing facilities configure custom leggings across three distinct lifestyle vectors dominant throughout Massachusetts:
Catering to luxury wellness enclaves in the Seaport District, Beacon Hill, and Newton. Garments require ultra-soft, peached "naked-feel" hand-feel with 0% opacity under intense studio lighting. We utilize air-jet texturized micro-nylon with high spandex ratios (up to 25%), bonded high-waist waistbands that eliminate rollover during reformer movements, and discreet internal card pockets.
Engineered for competitive collegiate track clubs, rowers, and marathon contenders battling coastal winds. We weave thermo-insulating hollow-core fibers for autumn/winter runs that trap warm boundary-layer air while actively shunting sweat outward. Integrated 360-degree high-lumen retroreflective transfer branding ensures safety during early-morning training along Memorial Drive.
Aligned with Boston’s academic, tech, and medical workforce walking from South Station to Kendall Square. These crossover pieces merge performance compression with structural aesthetics. We manufacture custom ribbed textures, discreet hip contour seams, and matte anti-snag finishes that pair seamlessly under fleece jackets and oversized technical coats.
For executive sourcing directors weighing fabric economics, product failure rates, and consumer retention, the architectural distinction between standard cut-and-sew manufacturing and seamless circular engineering is fundamental. The matrix below illustrates our testing benchmarks conducted under ASTM and AATCC standards.
| Engineering Attribute | Traditional Cut-and-Sew Leggings | Our Circular Seamless Technology | Commercial Value for Boston Brands |
|---|---|---|---|
| Fabric Waste Rate | 18% – 24% (marker cutting scraps) | < 3.5% (tubular yarn feeding) | Reduces carbon footprint; elevates sustainability narrative for eco-conscious New England buyers. |
| Chafing & Pressure Points | Multiple 4-thread flatlock seams along leg | 100% seam-free leg tube; smooth crotch gusset | Eliminates inner-thigh friction during high-mileage running; vastly reduces customer return rates. |
| Targeted Compression | Requires sewn-in contrast panels | Programmed yarn density shifts on same tube | Achieves medical-grade graduated compression (15–20 mmHg) without bulky, restrictive stitches. |
| Tensile Elastic Recovery | 82% recovery after 50 cycles | 96.4% recovery (ASTM D3107) | Prevents bagging at the knees and waist sagging over prolonged high-intensity workout routines. |
| Squat-Proof Opacity Test | Dependent on fabric weight and stitch stretch | 32-Gauge multi-feed high-density weave | 100% non-see-through rating even at maximum stretch extension during deep squats and yoga lunges. |
In accordance with Massachusetts environmental initiatives and the demanding sustainability standards of coastal US consumers, our activewear manufacturing processes prioritize circularity. We source high-tenacity post-consumer recycled polyamide (certified GRS nylon from recycled fishing nets and industrial plastic waste) and melt-spun bio-based elastane derived from renewable agricultural feedstocks.
Furthermore, traditional garment dyeing consumes extensive water reserves and energy. In our modernized facility, we utilize solution-dyeing (dope-dyeing) techniques for synthetic filament yarns where pigments are integrated directly into the polymer melt prior to extrusion. This results in superior colorfastness against chlorine, heavy sweat, and salt spray (Grade 4.5+ on the AATCC 8 scale), eliminating downstream toxic wastewater discharge while preserving saturated color brilliance across decades of laundering.
Combining industrial scale with artisanal finishing. We eliminate trading markups, deliver transparent technical auditing, and protect your proprietary brand patterns.
Every single batch undergoes dimensional stability checks, four-needle burst testing, and color-bleed evaluation before sealing into export cartons.
Our pattern masters convert 2D sketches or physical master samples into digitized 3D Clo3D renders and Santoni knitting software within 48 hours.
Complete custom branding ecosystem: heat-pressed holographic care labels, woven waist damask tags, custom FSC-certified swing tags, and frosted biodegradable polybags.
Direct DDP (Delivered Duty Paid) shipping corridors into Port of Boston (Conley Terminal) or express air consignments directly to Logan International Airport.
Everything you need to know regarding minimum order thresholds, US customs compliance, testing standards, and ODM turnaround times.
Partner directly with an enterprise activewear factory equipped with Santoni seamless machinery, in-house laboratory testing, and comprehensive private-label branding solutions. Request our full OEM/ODM product catalog, physical swatch cards, and instant wholesale quotation.
