Engineered through precision cut-and-sew craftsmanship, seamless knitting technology, and high-tenacity flatlock construction. Fully customizable for private labels, athletic federations, and wholesale distributors.
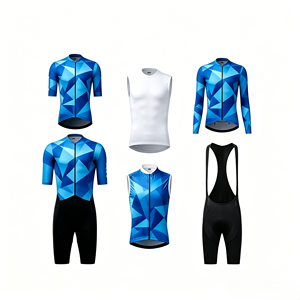
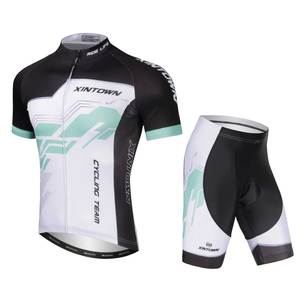
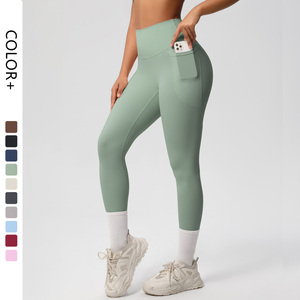
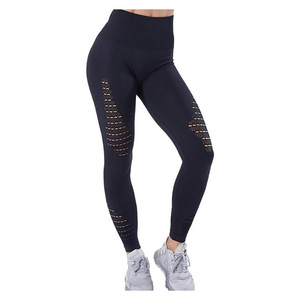
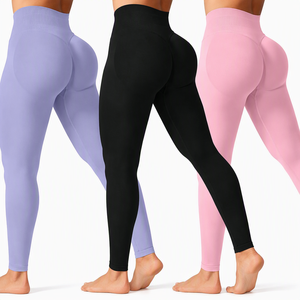
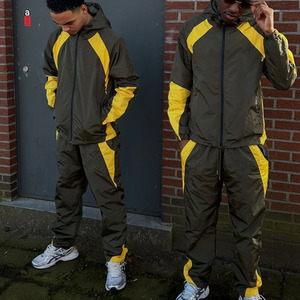
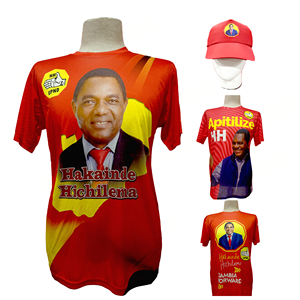
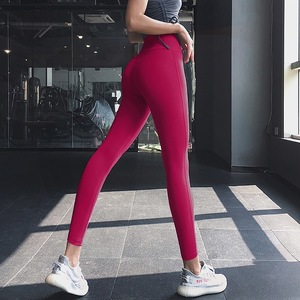
The international athletic apparel industry has shifted radically toward high-complexity functional engineering. In the modern B2B sportswear sector, cut and sew manufacturing is no longer a simple labor aggregation process; it is a meticulous, science-driven discipline involving dynamic mechanical stretch ratios, anisotropic yarn behavior, computational pattern grading, and climate-specific moisture permeability. As global fashion and performance brands diversify their manufacturing hubs to optimize supply chain resilience, Malaysia has emerged as a premier Southeast Asian center of excellence for precision athletic apparel manufacturing and international exports.
Operating in strategic industrial corridors connected directly to world-class logistics gateways such as Port Klang and Penang Port, our OEM/ODM facilities combine advanced CAD/CAM automated fabric-spreading systems, computerized laser cutting tables, and specialized stitching cells. Unlike traditional basic garment sewing, our dedicated cut and sew assembly lines are optimized for technical knit substrates ranging from high-gauge nylon/spandex interlocks to specialized hydrophobic warp-knit meshes. By executing rigorous quality assurance protocols that bridge raw yarn procurement to finished pre-pack cartons, our operations empower athletic brands, racing teams, tournament organizers, and corporate distributors worldwide to deploy market-leading sportswear collections with uncompromising dimensional stability and seam integrity.
Digital grading using Gerber and Lectra CAD suites. Every panel seam line is configured around musculoskeletal movement vectors to eliminate drag, friction blisters, and premature fabric fatigue.
Equipped with specialized high-speed Yamato and Juki flat-seaming machines. Produces smooth, skin-flush seams capable of withstanding 220N lateral tensile pull forces without unraveling.
High-definition industrial transfer printers utilizing eco-certified Swiss inks. Yields razor-sharp chromatic fidelity at 1200 DPI, complemented by ultrasonic seam welding and heat-sealed reflective taping.
Manufacturing high-performance sportswear for Malaysia, Singapore, Indonesia, and the broader ASEAN region demands an acute chemical and structural understanding of tropical equatorial climates. Operating in environments where relative humidity frequently exceeds 85% and ambient temperatures consistently hover between 30°C and 35°C renders conventional western synthetic garments unwearable due to sweat saturation, thermal entrapment, and severe chafing. As an established OEM/ODM exporter rooted in Malaysia, our engineering teams customize apparel architecture specifically for these rigorous localized conditions.
Engineered for endurance runners and urban fitness clubs across Kuala Lumpur, Johor Bahru, and Penang. We integrate hydrophilic cross-section microfibers (Coolmax/DryFit structures) with micro-mesh laser perforation under arms and along spinal gutters to maximize continuous evaporative cooling.
A surging multi-billion-dollar domestic and regional demographic. We manufacture loose-fit yet aerodynamically sleek tunics, extended drop-tail hem shirts, high-coverage ergonomic sports hijabs, and non-clinging, double-layer squat-proof leggings tailored for Muslimah athletes and lifestyle enthusiasts.
Custom multi-panel team wear designed for prestigious regional events such as Le Tour de Langkawi, standard chartered city marathons, and badminton league federations. Each garment incorporates UPF 50+ UV chemical dipping, quick-drying salt-water resistant thread, and high-visibility 3M reflective accents.
The macroeconomic environment governing Southeast Asian apparel manufacturing is undergoing a profound structural evolution. Sourcing directors from North America, Europe, Oceania, and regional ASEAN hubs are actively executing "China+1" and "China+2" supply chain diversification strategies. In this context, Malaysia offers unique structural advantages: high compliance with international labor standards (ESG), robust intellectual property protection, English-proficient engineering teams, and preferential duty-free tariff regimes under mega-trade pacts including the Regional Comprehensive Economic Partnership (RCEP) and the Comprehensive and Progressive Agreement for Trans-Pacific Partnership (CPTPP).
Furthermore, modern brand sourcing is trending toward agile, mid-tier batch production. The era of rigid 50,000-piece single-color MOQs is being superseded by flexible cut and sew programs that permit dynamic seasonal reorders and rapid drop-shipping. Our factory combines localized fabric knitting partnerships with vertical in-house cutting, digital sublimation, and automated packing to facilitate low-risk product line rollouts. Additionally, sustainability mandates have triggered massive demand for circular textiles; our facilities actively process certified Recycled Polyethylene Terephthalate (rPET) derived from post-consumer plastic bottles and OEKO-TEX Standard 100 Class I certified dyes, aligning your athletic collections with rigorous global environmental frameworks.
| Performance Characteristic | Pro Cycling / Aero Kits | Seamless Athleisure & Leggings | Sublimated Event & Team Tees | Patchwork Outerwear / Tracksuits |
|---|---|---|---|---|
| Fabric Composition | 82% Poly, 18% Elastane (140 GSM) | 75% Polyamide 6.6, 25% Spandex (240 GSM) | 100% Micro Interlock Poly (135 GSM) | 100% Taslon Ripstop Poly + DWR (110 GSM) |
| Seam Technology | Ultrasonic weld + 3-Needle Coverstitch | 4-Needle 6-Thread Flatlock (ISO 607) | High-Elastic Overlock (ISO 504) | Twin-Needle Bound Edge + Taped Seams |
| Moisture Management | Wicking Speed < 1.2 sec (AATCC 79) | Moisture Vapor Perm > 8000 g/m²/24h | Hydrophilic Cross-Capillary DryFit | Breathable Mesh Back Venting Core |
| Color Fastness | Grade 4.5+ Sublimation (ISO 105-C06) | Grade 4.0+ Reactive Vat Dyeing | Grade 4.5+ Swiss Disperse Ink | Grade 4.0+ Solution-Dyed Filament |
| Target Application | Road Races, Gran Fondos, Criteriums | Yoga, Crossfit, Modest Athleisure | Marathons, Sports Leagues, Campaigns | Warmup Training, Sideline, Streetwear |
Everything sourcing managers, brand founders, and apparel merchandisers need to know regarding manufacturing lead times, MOQs, technical customization, and export customs.
Our flexible manufacturing model accommodates varying order tiers based on construction type. For full-dye digital sublimation sportswear (e.g., cycling jerseys, soccer uniforms, marathon shirts), our standard MOQ is 50 to 100 pieces per design with flexible size breakdowns. For complex cut and sew styles requiring custom mill-dyed nylon/spandex textiles or unique Pantone pantone dip approvals (such as high-waist squat-proof leggings and multi-panel tracksuits), our MOQ typically begins at 300 to 500 pieces per colorway.
Malaysia is an active signatory to prominent free trade agreements, notably RCEP, CPTPP, and bilateral ASEAN trade pacts. Sourcing from our Malaysian facilities allows qualifying buyers in Australia, New Zealand, Japan, the UK, Canada, and ASEAN member states to benefit from zero or significantly reduced import customs tariffs under Form E, Form D, and other preferential Certificates of Origin (CO). This delivers substantial cost margins over sourcing from non-pact manufacturing territories.
Upon tech-pack validation, digital vector artwork confirmation, and fabric selection, sample production typically requires 7 to 12 working days. We produce full counter-samples including branding labels, hang tags, and custom silicone trims for client sign-off. Bulk mass production generally requires 3 to 5 weeks following Pre-Production (PP) sample approval, depending on aggregate volume, embellishment complexity, and current mill scheduling.
Yes, turnkey private label execution is a pillar of our ODM/OEM operation. We manufacture custom heat-transfer neck tags, high-density woven damask labels, organic cotton care labels, custom branded zipper pullers, branded hangtags with scannable UPC/EAN barcodes, and eco-friendly frosted biodegradable EVA polybags ready for direct Amazon FBA or multi-door retail fulfillment.
Absolutely. While comprehensive tech packs accelerate sampling, our in-house ODM pattern development department can reverse-engineer any physical benchmark garment or translate conceptual hand-drawn sketches and reference images. We establish graded digital spec sheets, generate CAD marker files, and advise on optimal fabric weight, elasticity tolerances, and panel layout.
Our quality control protocols comply strictly with ISO 9001 and AQL 2.5 (Acceptable Quality Limit) standards. Every order undergoes 4-stage inspection: (1) Raw fabric 4-point system testing for color fastness, shrinkage, and torque; (2) Inline cutting and stitching checks for dimensional conformity; (3) Post-assembly stress tests including 4-way stretch rebound, squat-proof opacity testing, and seam tear elongation; (4) 100% pre-pack visual inspection.
Eliminating the costly markups and communication gaps associated with trading agents, our direct manufacturing infrastructure ensures total transparency and tight configuration control from raw yarn spinning to container dispatch.
We review your artwork, confirm PMS color matching codes, test lab-dip strike-offs under standard D65 light booths, and digitally approve CAD marker nestings to optimize material yield and lower unit costs.
Computerized fabric spreading ensures zero longitudinal fabric tension before high-precision CNC blade cutting. Printed panels undergo thermal transfer at 210°C before being routed to dedicated Juki flatlock stitching cells.
Finished apparel passes metal needle detectors, dimensional tolerance audits, and garment wash endurance trials. Export cargo is packaged in heavy-duty export cartons and routed through Port Klang via sea or air freight (FOB, CIF, or DDP).
