
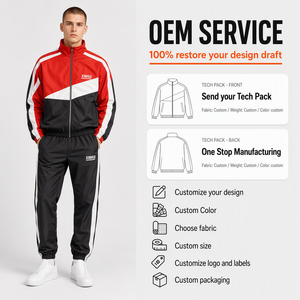
Manufactured under strict ISO/AQL tolerances with moisture-management polymers, thermal retention meshes, and four-way ergonomic elasticity.
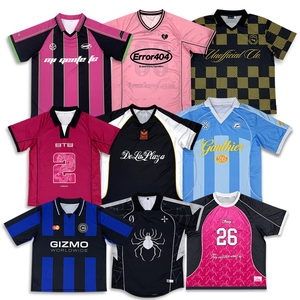
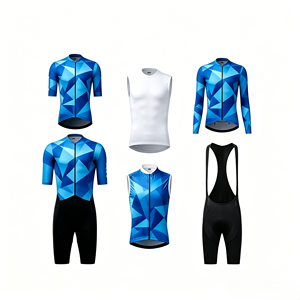
A rigorous examination of fabric mechanics, environmental micro-climates, and localized commercial delivery models across Greater London and European distribution channels.
Standard circular cotton fibers absorb up to 8% of their dry weight in perspiration, swelling and collapsing cross-sectional airflow. Our engineered performance fabrics utilize extruded modified cross-section polyester (cross-shaped, trilobal, or multichannel profiles).
These configurations create microscopic channels that pull liquid sweat outward through spontaneous capillary pressure, maximizing the surface surface evaporation area across our high-output garments.
London athletes face distinct atmospheric challenges: variable oceanic precipitation matched with cool, damp temperatures (averaging 55–85% RH). In these settings, rapid wicking must be balanced with controlled evaporative cooling.
Our dual-surface textile weaves integrate hydrophobic inner faces (polypropylene/micro-poly) that push moisture directly to a quick-drying hydrophilic exterior layer, preventing the severe post-exercise hypothermic chilling common in standard workout apparel.
Synthetic filaments naturally bind lipid molecules found in human apocrine perspiration, creating an environment ripe for microbial growth and persistent smells. To solve this, our London-destined exports feature non-leaching silane quaternary ammonium compounds or silver-ion matrix finishes.
These treatments rupture bacterial cell membranes on contact without irritating human skin, keeping shirts fresh across extended wear and repeated industrial laundering.
How specialized performance shirts match the operational demands of institutional, competitive, and boutique procurement bodies in London.
Spanning the Southern League, Isthmian divisions, and the amateur Sunday football circuits in Hackney Marshes and Regent's Park. Teams require uniforms with high puncture resistance against pitch sliding, sharp dye-sublimated graphics for commercial sponsors, and moisture-wicking fabrics that hold up through grueling 90-minute matches in heavy UK rain.
Centered around high-density athletic markets in Shoreditch, Soho, Battersea, and Canary Wharf. These venues focus on private-label lines made from silky, high-stretch poly-spandex blends. Garments must have zero transparency, reliable anti-chafing seams, and an upscale, understated matte visual style.
High-volume programs such as the London Marathon, central charity cycle rides, and City of London financial wellness leagues. Buyers prioritize bulk consistency, dependable size runs across broad demographics, and high-contrast reflective detailing for pre-dawn and evening commutes.
A reference guide for sportswear brand managers, procurement directors, and sports uniform coordinators evaluating technical trade-offs.
| Material Engineering | Composition & Weight | Wicking Dynamics | Durability / Laundering | Optimal UK Commercial Use |
|---|---|---|---|---|
| Micro-Pinhole Poly Mesh | 100% Interlock Poly (135–150 GSM) | Exceptional (Evaporative capillary draw) | High resistance to snagging; washes at 40°C | Club Football, Rugby, Cycling Teamwear |
| Bushed Spandex Poly | 88% Polyester, 12% Spandex (180–220 GSM) | Medium-High (Multidirectional recovery) | Retains original elasticity past 75+ cycles | Gym Base Layers, Running Tops, HIIT Lines |
| Warp-Knit Active Nylon | 80% Nylon 6.6, 20% Elastane (210 GSM) | Rapid sweat absorption with smooth hand-feel | High abrasion resistance against weights & turf | Premium Private Label, Cross-Training Kits |
| GRS Recycled Poly Blend | 92% rPET, 8% Elastane (160 GSM) | Engineered micro-porous wicking profile | Low carbon footprint; wash testing verified | Corporate Green Programs, Marathon Kits |
Emerging structural changes shaping how institutional sports apparel buyers make contract decisions.
UK consumer sentiment and corporate ESG mandates are shifting performance lines toward GRS (Global Recycled Standard) verified rPET. Recycled filaments made from ocean-bound bottles must deliver the exact same surface tension and moisture dispersal rates as virgin polyester without driving up unit costs.
London buyers increasingly move away from flashy neon sports designs in favor of refined, street-ready silhouettes. Drop shoulders, boxy profiles, muted earth tones, and tonal silicone logos mean shirts must work just as well on a Northern Line commute as they do in an evening workout.
By cutting out domestic trading intermediaries, UK buyers gain direct access to raw manufacturing floors. Working directly with factory teams provides clear AQL 2.5 audit trails, accurate lead-time schedules, and transparent lab-dip signoffs across the entire production cycle.
Full manufacturing execution in Sialkot, Pakistan—a world-class hub for athletic goods—delivering directly into London, Essex, and UK logistics distribution centers.
From pattern drafting and fabric spreading to precision sublimation, multi-head embroidery, and final packing, every single order is produced under one roof. This internal setup protects quality control and prevents the delays common with outsourced subcontracting.
We eliminate variances between initial samples and final bulk orders. The pre-production sample approved by your team serves as our locked production benchmark. Fabric lots, dye formulas, seam tensions, and dimensions are strictly measured against agreed tolerances.
We handle all shipping paperwork, commercial documentation, and airway/ocean bills for clear customs clearance at Heathrow, London Gateway, and Felixstowe. Choose FOB, CIF, or DDP terms for seamless delivery straight to your regional depot.
Detailed operational answers covering MOQ flexibility, British wash compliance, import documentation, and lab-dip turnarounds.
Access custom moisture-wicking apparel with consistent sample matching, competitive factory pricing, and full technical documentation for your brand.