Browse our factory-direct performance activewear lines designed for tier-1 athletics brands, cycling teams, and eco-conscious private label labels. Every design accommodates custom post-consumer rPET, recycled nylon (ECONYL® grade), and non-toxic water-based sublimation systems.
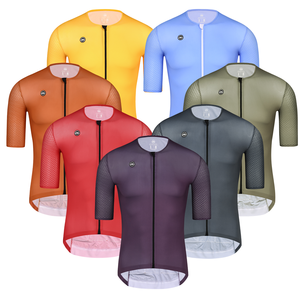
Aero-contoured cut using 110-135 GSM micro-perforated recycled filament polyester with OEKO-TEX® non-fade sublimation.
Product Specification →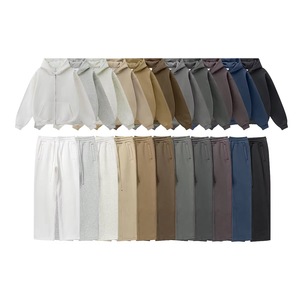
Heavyweight 380-420 GSM brushed circular fleece made from 70% organic cotton and 30% GRS post-consumer recycled poly.
Product Specification →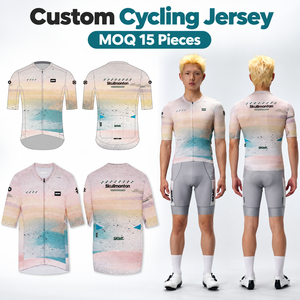
Ultralight breathable mesh featuring dynamic capillary action wicking and 4-way mechanical elasticity for road race ergonomics.
Product Specification →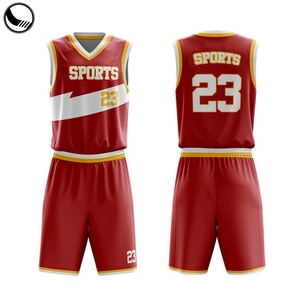
Double-layer reversible dual-knit pinhole mesh with anti-snag coating and chlorine/sweat-resistant dye transfer.
Product Specification →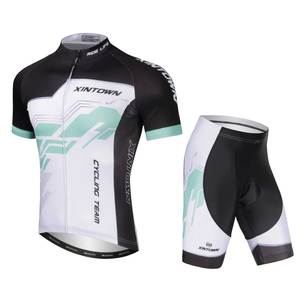
Bonded thermal edge finishes, multi-density high-impact chamois pad, and friction-reducing seamless side-paneling.
Product Specification →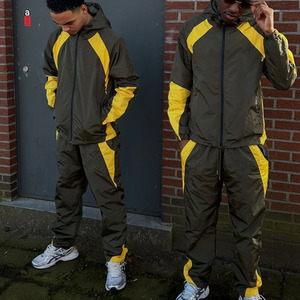
High-density recycled woven shell with PFC-free DWR water repellent coating and internal breathable mesh lining.
Product Specification →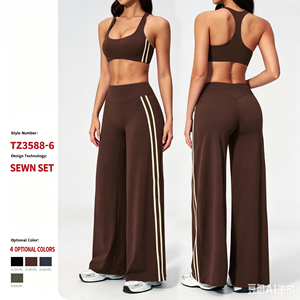
Santoni-knitted seamless construction, squat-proof 280 GSM high-interlock stretch with targeted micro-rib support zones.
Product Specification →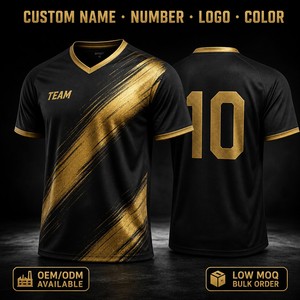
145 GSM honey-comb moisture extraction knit, reinforced flatlock seams, customized club badges, and athletic cut.
Product Specification →As international sustainability mandates such as the European Union's Corporate Sustainability Due Diligence Directive (CSDDD) and Extended Producer Responsibility (EPR) take effect, global activewear buyers face tightening traceability standards. Modern apparel sourcing requires full chain-of-custody verification from chip to spinning, knitting, and finished assembly.
Our manufacturing cluster leverages state-of-the-art circular knitting machines and Santoni seamless systems to process recycled polyester (rPET) derived from post-consumer plastic bottles, alongside recycled Polyamide 6 and 6.6 (regenerated nylon ocean waste). By pairing closed-loop water treatment facilities with non-toxic, Azo-free Italian dye inks, we ensure that performance attributes—hydrophilic wicking, mechanical rebound stretch, thermal retention, and ultraviolet defense—match or exceed virgin synthetic formulations while lowering carbon emissions by up to 45% per production run.
Stay ahead of consumer demand and evolving environmental standards with strategic intelligence compiled by our textile R&D engineers.
Traditional elastane-blend garments present severe mechanical recycling bottlenecks during post-consumer sortation. Next-generation apparel procurement focuses heavily on 100% monomaterial constructions, utilizing mechanical-stretch polybutyl terephthalate (PBT) and bio-based elastic polyesters to achieve pure recycling loops without elastane breakdown penalties.
Tier-1 importers across North America and Europe are shifting procurement contracts to suppliers who provide granular batch traceability. Future purchase orders integrate batch-level QR codes linking directly to Transaction Certificates (TCs), carbon footprint metrics, and chemical testing reports complying with REACH and ZDHC standards.
Seamless athletic wear reduces fabric cut-and-sew scrap loss from 18% down to under 3%. Advances in 3D multi-density micro-loop knitting allow compression gradient mapping directly into leggings and sports tops, eliminating bulky abrasive seaming while deploying variable air permeability zones across the human thermal map.
Evaluate structural and performance parameters to select the ideal recycled composite for your private-label sportswear portfolio.
| Fabric Classification | Primary Substrates | GSM Range | Core Performance Attributes | Typical Target Apparel |
|---|---|---|---|---|
| rPET Interlock Quick-Dry | 100% Post-Consumer Recycled Poly | 120 - 160 GSM | Capillary moisture wicking, UV50+ defense, rapid evaporation | Pro Cycling Jerseys, Soccer Kits, Running Singlets |
| Regenerated Nylon Tactel / Spandex | 78% r-Polyamide, 22% Roica Elastane | 220 - 290 GSM | Ultra-soft buttery hand-feel, zero-transparency squat proof, 4-way recovery | High-Waist Yoga Leggings, Athleisure Tights, Biker Shorts |
| Heavy Recycled French Terry / Fleece | 65% Organic Combed Cotton, 35% rPET | 340 - 450 GSM | High thermal insulation, anti-pilling compact spun face, low-shrink wash | Streetwear Hoodies, Athletic Joggers, Winter Training Sets |
| PFC-Free DWR Recycled Ripstop | 100% Recycled Nylon 6 (Fishery Waste) | 75 - 110 GSM | Windproof, hydrostatic head 5,000mm rating, ultralight packability | Performance Windbreakers, Trail Running Shells, Running Pants |
| Dual-Knit Air Pinhole Mesh | 100% GRS Microfilament Polyester | 140 - 180 GSM | Maximized air exchange throughput, tear-resistant warp-knitted mesh | Reversible Basketball Uniforms, Field Hockey Jerseys |
Combining industrial textile engineering with vertical control to deliver dependable delivery timelines, custom tooling, and strict international compliance.
By cutting out intermediate trading houses, you communicate directly with senior pattern makers, dyeing engineers, and production line directors. This guarantees rapid tech pack iteration, clear unit costing, and responsive line agility.
Our quality control protocol inspects incoming yarn tenacity, conducts 4-point fabric roll analysis, executes inline stitching tension checks, and performs rigorous post-laundry shrinkage and color migration audits before release.
From biodegradable cornstarch polybags and FSC-certified seed-paper hangtags to heat-seal satin neck tags and master carton barcode serialization, we deliver complete turnkey logistics ready for retail distribution and Amazon FBA receipt.
Clear answers to operational and technical inquiries regarding bulk recycled activewear manufacturing.
