Browse our core manufacturing catalog spanning engineered seamless yoga leggings, high-waisted shaping pants, athletic compression base layers, and professional sublimated sports garments produced to rigorous international benchmarks.
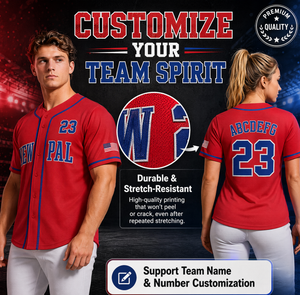
Engineered 180–220 GSM moisture-wicking interlock, full-bleed Italian dye sublimation, anti-pilling, and reinforced double-needle plackets.
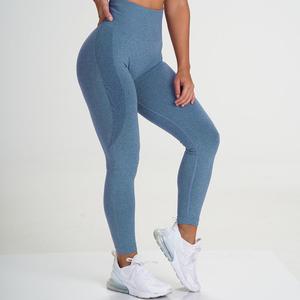
SANTONI circular knit 320 GSM micro-ribbed compression waistband, 100% squat-proof 4-way interlock, and diamond crotch gusset.
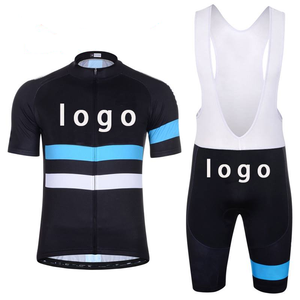
Aerodynamic matrix mesh side-panels, YKK auto-lock hidden zipper, reflective rear accents, and anti-slip silicone waist gripper.
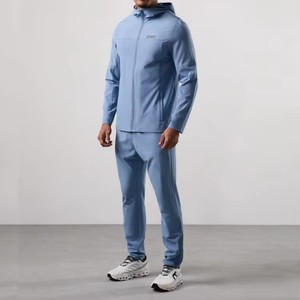
DWR coated nylon ripstop shell, breathable poly-mesh lining, taped water-resistant seams, and adjustable bungee toggles.
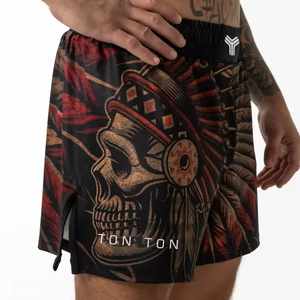
High-tensile tear-resistant microfiber, 4-way stretch inner crotch flex panel, reinforced split outseam, and hook-and-loop closure.
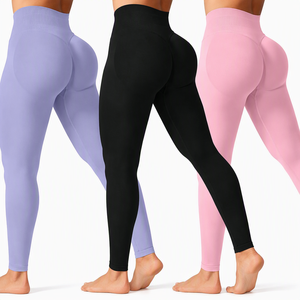
Ultra-soft 90% Polyamide 10% Elastane blend, body-mapped jacquard ventilation panels, anti-chafing ergonomic construction.
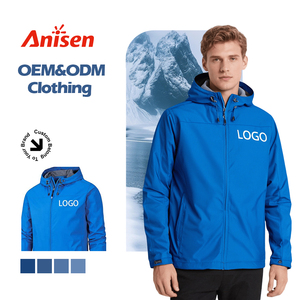
3M Scotchlite reflective piping, 5000mm hydrostatic head waterproof rating, wind-blocking collar, and ergonomic raglan sleeves.
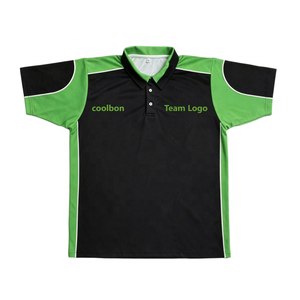
Birdseye jacquard pique knit, UV SPF 50+ rating, laser-cut ventilation underarms, anti-curl knitted collar, and customized pearl buttons.
A B2B sourcing director's breakdown of yarn denier, circular knitting gauges, elastane recovery hysteresis, and anatomical tummy control construction.
We utilize micro-denier Nylon 6.6 (polyamide) cross-knit with Creora® or Lycra® high-power spandex (75D/48F or 40D/34F). This configuration provides a soft, buttery tactile hand while ensuring maximum tensile elasticity. The molecular structure of Polyamide 6.6 delivers superior abrasion resistance (>50,000 rubs Martindale), preventing pilling and seam degradation during high-intensity training cycles.
Tensile Recovery > 98%Our high-rise waistbands (ranging from 10cm to 13cm in height) feature dual-layer cross-tension zoning. By incorporating an internal bonded mesh or a reinforced micro-rib structure, the waistband achieves graduated abdominal support without requiring rigid elastic inserts that cause uncomfortable skin indentation or roll-down during deep squats and yoga transitions.
Zero-Slip Dual MatrixEliminating friction points is essential for professional gym tights. Our factory operates automated Yamato 4-needle 6-thread flatlock stitching stations utilizing textured filament micro-threads (14–16 stitches per inch). For luxury minimalist collections, we deploy heat-activated thermoplastic polyurethane (TPU) ultrasonic taped seams to produce entirely stitch-free hemline profiles.
Flat Seam Bursting > 120 PSIEvaluate production costs, minimum orders, hand-feel, compression levels, and optimal target markets across different manufacturing methods.
| Manufacturing Technology | Fabric Composition & GSM | Compression & Elasticity | Typical MOQ & Lead Time | Ideal Market Application |
|---|---|---|---|---|
| Circular Seamless (Santoni Top2 Fast) | 88% Polyamide 6.6 / 12% Spandex (280–340 GSM) | High targeted zoning; 3D knitted micro-compression | 500–1,000 pcs / colorway Sampling: 10–12 Days |
Gymshark-style contouring leggings, high-impact yoga, athleisure collections. |
| Cut & Sew Interlock (4-Needle 6-Thread) | 75% Nylon / 25% Spandex Brushed (220–260 GSM) | Uniform medium-firm support; buttery, peach-skin feel | 100–300 pcs / style Sampling: 7 Days |
Lululemon Align-type yoga pants, studio Pilates, everyday premium athleisure. |
| Thermobonded Stitch-Free | 71% Polyamide / 29% Extra Life Lycra (210 GSM) | Sleek second-skin; zero chafe seam construction | 800–1,500 pcs / style Sampling: 14 Days |
Luxury athletic couture, endurance marathon tights, triathlon base layers. |
| Custom Sublimated Interlock | 82% Performance Poly / 18% Elastane (240–280 GSM) | Moderate athletic recovery; unlimited graphic placement | 50–100 pcs / style Sampling: 5–7 Days |
CrossFit team tights, branded merchandise, artistic printed fitness tights. |
Navigating supply chain geopolitical transitions, circular material mandates, micro-batch responsiveness, and digital fabric traceability.
Global regulatory frameworks (such as the EU Ecodesign Directive) are accelerating the transition from virgin petrochemical textiles to certified Global Recycled Standard (GRS) yarns. Tier-1 brands are transitioning from generic recycled polyester to high-tenacity recycled Nylon 6 yarn synthesized from abandoned fishing nets (ECONYL®) and industrial yarn scrap, demanding verified blockchain chain-of-custody documentation.
GRS & OEKO-TEX Standard 100The traditional 6-month seasonal apparel calendar is being superseded by continuous drop models. Modern activewear retailers rely on Chinese manufacturing partners capable of initial test runs of 100–300 units per SKU, followed by rapid 15-day replenishment cycles driven by real-time POS data. Our optimized lean production lines enable agile brand owners to minimize deadstock depreciation risks.
Lean Kanban ProductionTo mitigate tariff volatility, leading brand procurement teams partner with vertically integrated manufacturers managing dual hub structures. By conducting technical fabric development, automated precision laser cutting, and initial sampling in China while coordinating regional assembly hubs, brands achieve optimal tariff classifications alongside world-class synthetic textile consistency.
Customs & Duty PlanningCombining over 15 years of technical textile mastery with ISO 9001 certified inline quality assurance, zero-compromise squat-proof testing, and full private-label customization.
Every batch of knitted fabric undergoes strict back-stretch photometric opacity checks (lux-meter tests) to guarantee zero transparency during extreme 90-degree flexion under gym lighting.
Accelerate fit sample development with CLO 3D virtual prototyping. We calibrate precise fabric stretch physics before cutting a single yard of fabric, reducing sample revision rounds by 60%.
Arrive retail-ready with custom woven labels, silicone heat-press interior wash tags, FSC-certified hangtags, QR-code inventory stickers, and biodegradable frosted ziplock polybags.
Direct communication with bilingual apparel textile engineers. Physical samples couriered via DHL/FedEx within 7–10 working days of approved technical drawings and lab dips.
Transparent production milestones designed to eliminate defect propagation from yarn cone spinning through pre-shipment ocean container loading.
Fabric composition review, Pantone spectrophotometer color-matching (Delta E < 0.8), stretch ratio verification, and digital pattern grading across sizes XXS to 4XL.
Physical sample cutting, live model tension testing, 4-point stitch stretch evaluation, and waistband recovery measurement after 5 consecutive laundry wash cycles.
Automated tension-free fabric relaxation (24 hours minimum), computerized vacuum knife cutting for micro-tolerance panel alignment, or circular 28-gauge Santoni seamless knitting.
Flatlock tension testing (pulling seams to 150% maximum expansion), waistband elastic torque inspection, gusset reinforcement auditing, and defect tracing at station level.
Randomized AQL 1.5/2.5 pre-shipment inspection, needle detector metal screening, barcoded polybag verification, and export carton burst-strength certification.
Direct, transparent answers regarding manufacturing minimums, sample lead times, testing protocols, private branding, and shipping incoterms.
Our standard MOQ for cut-and-sew custom leggings using our in-stock premium nylon/spandex or polyester/spandex performance fabrics is 100 to 200 pieces per style/colorway across multiple sizes. For completely custom yarn dyeing (bespoke Pantone matching) or Santoni circular seamless leggings, the standard production minimum is 500 to 800 pieces per colorway, with flexible sizing breakdown allowances.
We prevent fabric transparency through a three-tier quality control protocol: First, we specify a minimum yarn density threshold of 240 to 320 GSM using tight 28G/32G double-knit interlock weaving machines. Second, we verify black and deep-shade yarn dyeing penetration to eliminate white core grin-through under extreme elongation. Third, every production lot is subjectedively tested using a 90-degree flexion squat test over calibrated contrast patterns under 1000 lux illumination.
Yes. While full tech packs expedite production, our in-house ODM engineering department frequently develops commercial styles from reference samples, high-resolution photographs, or design concept sketches. We will produce a complete computerized grading specification sheet, fabric swatch card, and 3D fit visualization for your formal approval prior to cutting sample garments.
Fit and counter-sample development typically takes 7 to 10 working days following tech pack confirmation and fabric swatch selection. Bulk production typically spans 25 to 35 business days from the formal confirmation of the golden pre-production (PP) sample and deposit receipt. We also offer expedited express sampling and air cargo dispatch for time-sensitive product drop schedules.
Our manufacturing facilities and upstream dyeing mills maintain OEKO-TEX Standard 100 Class I (safe for skin contact), Global Recycled Standard (GRS 4.0), HIGG Index sustainability reporting, and BSCI / SEDEX social compliance auditing certifications. Comprehensive chemical laboratory testing reports (REACH, formaldehydes, azo dyes, heavy metals) are available on demand for all commercial orders.
We support FOB (Shanghai / Ningbo / Shenzhen), CIF, CFR, and hassle-free DDP (Delivered Duty Paid) door-to-door options via sea freight, express air courier (DHL, FedEx, UPS), and dedicated air cargo forwarders directly to your 3PL fulfillment warehouse or Amazon FBA depot. Payment terms are typically 30% deposit with 70% balance payable upon completion of pre-shipment AQL inspection.
Send us your tech pack, reference image, or physical garment requirements. Our senior activewear textile engineers will provide free material consultations, cost breakdowns, and a dedicated sampling timeline within 1 business day.
