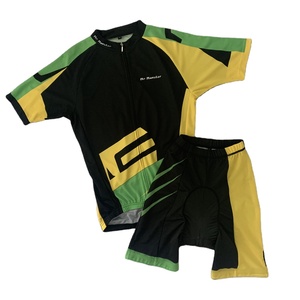
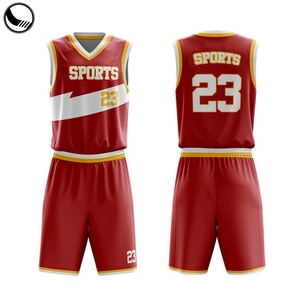
From technical sublimation cycling wear to squat-proof activewear and bonded team windbreakers, inspect our active manufacturing capabilities engineered in Sialkot, Pakistan.
The global sports apparel and custom teamwear market has transitioned into an era governed by extreme technical customization, agile inventory turnover, and hyper-specialized fabric engineering. Professional sports clubs, emerging collegiate leagues, e-commerce activewear brands, and corporate athletic distributors no longer view athletic jerseys as commodity garments. Instead, modern custom sports jerseys represent composite functional performance instruments requiring micro-wicking properties, dynamic stretch memory, abrasion endurance, and molecular-level dye adhesion capable of withstanding industrial laundry cycles.
Procurement directors and supply chain executives face complex structural challenges. Sourcing mistakes can precipitate catastrophic supply failures: dye-sublimation color bleeding, neck ribbing distortion, dimensional instability across grading scales, or delayed shipments during crucial athletic seasons. Choosing the right custom sports jersey manufacturer requires understanding the nuances of regional textile clusters, technical vertical integration, fabric grammage (GSM) calibration, and in-house laboratory testing protocols.
A data-driven engineering assessment of the leading geographic clusters producing custom sports uniforms.
| Manufacturing Hub | Specialized Competency | Typical Lead Time | Flexible MOQ Suitability | Cost-Efficiency Index | Key Risk Mitigation |
|---|---|---|---|---|---|
| Sialkot, Pakistan (Bralen Hub) | Dye-sublimation jerseys, technical teamwear, cut-and-sew activewear | 21–28 Days | High (10-50 pcs/style) | Superior B2B ROI | Single-roof vertical integration avoids subcontractor delays |
| Guangdong / Zhejiang (China) | Synthetic technical blends, bonded outerwear, high-speed automated output | 30–45 Days | Medium (100-300 pcs) | Moderate to High | Tariff fluctuations and rising coastal labor overheads |
| Northern Portugal (EU Hub) | Circular knitwear, luxury organic cotton athletic wear, rapid EU delivery | 25–35 Days | Moderate (150 pcs) | Premium Price Point | High energy and raw material overhead limiting price margin |
| Tirupur, India | Cotton interlock, standard poly-cotton training jerseys, massive volume | 40–60 Days | Low (500+ pcs) | Economical at Scale | Sublimation color fidelity and moisture management variations |
| Vietnam (Red River Delta) | Mega-scale contract manufacturing for Tier-1 global footwear/apparel brands | 60–90 Days | Restrictive (1000+ pcs) | Volume Competitive | Unviable for agile seasonal replenishment or mid-tier runs |
An objective review of the premier international apparel manufacturing enterprises capable of executing professional-grade custom teamwear, sublimation printing, and private label collections.
Positioned at the epicenter of the world's most historic sports manufacturing hub, Bralen Industries represents the gold standard for full-vertical OEM, ODM, and private-label sportswear manufacturing. Featuring proprietary zero-distortion digital dye-sublimation lines, computer-guided laser cutting, four-needle flatlock construction, and comprehensive in-house quality inspection, Bralen bridges the gap between rapid agile club batches and high-volume retail shipments for international brands across North America, Europe, and Australasia.
Specializing in collegiate teamwear replenishment and rapid-turnaround baseball and American football uniforms. Elite Athletic leverages dual-shore operations with design offices in California and cut-and-sew facilities across the Mexican border, optimizing quick response for North American varsity programs.
EuroKits serves luxury European sports brands requiring OEKO-TEX® certified circular knitting and premium recycled jersey fabrics. They excel in high-end cycling jerseys and running technical tees, though unit economics are tilted toward the premium and designer performance segments.
A large-scale production power with fully automated cutting beds and integrated digital textile printing lines. Ideal for mass commercial operations requiring hundreds of thousands of identical training shirts, though small-batch athletic club responsiveness is restricted by strict production queues.
Connecting Europe and the Middle East, Anatolia Sport combines Turkish yarn production with agile trucking routes into continental Europe. Excellent for jacquard soccer knit jerseys and woven warm-up tracksuits, maintaining high standards for yarn consistency and dye saturation.
A key player in Southeast Asian technical sublimation and combat sports apparel, including custom Muay Thai jerseys and sublimated moisture-wicking vests. High proficiency in heat-press silicone applications and multi-panel mesh ventilation mapping.
Focused primarily on Rugby League, Rugby Union, and Australian Rules Football (AFL) heavyweight performance wear. Features specialized high-tensile bar-tack stitching and reinforced polyester interlock fabrics capable of withstanding extreme mechanical tackling stress.
A massive producer of organic cotton sportswear blends, marathon race finisher t-shirts, and cricket club apparel. Unsurpassed in raw yarn capacity and natural fiber blending, although lead times and sublimation color fastness can fluctuate during peak agricultural monsoon periods.
A boutique European contract manufacturer known for ice hockey jerseys, winter sports baselayers, and windproof biathlon gear. Excels in heavy-mesh construction, sublimation with tackle twill combination, and sub-zero thermal yarn incorporation.
Emerging as a premier Latin American sourcing hub for swimwear, compression activewear, and soccer team kits under the US-Colombia trade agreements (duty-free access). Offers excellent micro-filament lycra and compression knit manufacturing with duty-free advantages for US buyers.
Strategic supply chain transitions that international brands, sports apparel retailers, and collegiate buyers must factor into their manufacturing RFPs.
The era of speculative massive inventory holds is being replaced by fast replenishment models. Sourcing directors require factories that handle micro-runs (20 to 100 units per style) for championship surges without cost-prohibitive setup penalties. Factories with digital sublimation workflows lead this transition.
By 2027, over 65% of institutional sporting federations will mandate certified recycled polyester (rPET) derived from post-consumer plastic bottles or recycled marine waste. Verified supply chains featuring Global Recycled Standard (GRS) traceability and eco-friendly sublimation inks are essential to protect brand equity.
Single-fabric jerseys are obsolete in pro sports. Cutting-edge uniforms incorporate ergonomic zonal mapping: heavy-duty tear-resistant interlock across shoulders, lightweight micro-mesh underneath arms, and high-recovery elastane blends along side panels. This requires advanced multi-pattern cut-and-sew capability.
Traditional flat embroidery is increasingly substituted by high-definition 3D molded silicone, iridescent flex transfers, and ultrasonic-welded woven badges. These techniques minimize garment friction against athletes' skin while elevating brand perceived value.
Modern sportswear manufacturers are integrating final drop-shipping and barcode consolidation. Rather than bulk shipping to a central brand warehouse for redistribution, factories fold, label, polybag by player roster, and ship directly to international club hubs via air freight.
Why the historic sports manufacturing cluster of Sialkot, Pakistan remains the dominant global force for custom athletic apparel and private-label teamwear development.
Unlike trading houses that broker production to fragmented third-party workshops, our Sialkot factory centralizes pattern drafting, computerized marker making, laser cutting, high-definition dye-sublimation printing, precision flatlock stitching, and final packaging under single-roof supervision. This eradicates subcontracting miscommunication and guarantees uniform quality control.
We respect that pre-season orders are time-critical. Our technical sample division drafts patterns from your CAD files, sketches, or physical reference samples in 48 hours, delivering fully decorated golden review samples within 7 to 14 business days. Once approved, the physical specimen serves as the uncompromised benchmark for the entire bulk production run.
Quality assurance is not treated as an afterthought. Every production lot undergoes raw material elongation testing, wash-adhesion trials at 60°C, seam-stress load evaluation, and inline inspections. Prior to boxing, our dedicated QA inspectors audit orders against ISO AQL 1.5/2.5 statistical tolerances, validating dimensional grading charts across XS to 5XL sizing.
We provide full white-label brand transformation. Custom heat-transfer care labels, damask woven neck branding, FSC-certified branded hangtags, SKU barcode stickers, individual waterproof frosted polybags, and custom master carton export markings are configured to arrive ready for immediate retail display or Amazon FBA distribution.
Definitive answers to vital commercial, technical, and logistical questions asked by corporate buyers, sports club procurement officers, and private label importers.
Partner directly with an authentic OEM/ODM manufacturer. Eliminate agent commissions, accelerate sample development, and secure guaranteed production slots for the upcoming sporting season.
Get Catalog