Engineered with micro-filament quick-drying textiles, reinforced 4-needle 6-thread ergonomic flatlock stitching, and ultra-vivid sublimation printing directly calibrated for athletic clubs, brand owners, and franchise distributors.
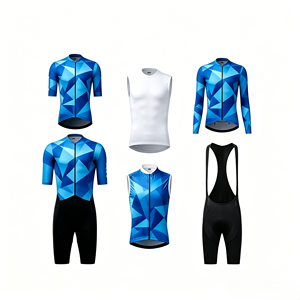
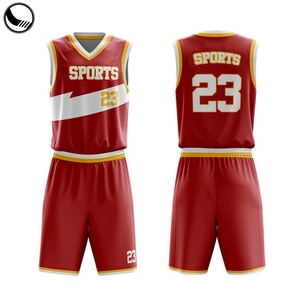
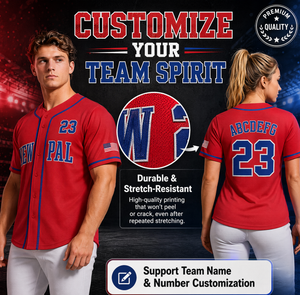
Modern cricket has undergone an unprecedented transformation over the past decade. The evolution from traditional five-day red-ball matches to high-velocity franchise leagues—such as the Indian Premier League (IPL), Pakistan Super League (PSL), Australia's Big Bash League (BBL), England’s The Hundred, and the USA's Major League Cricket (MLC)—has revolutionized athletic apparel requirements. Today's cricket kit is no longer a generic poly-cotton polo; it is an aerodynamically calibrated, biomechanically mapped piece of high-performance technical sports equipment.
Cricket apparel requires distinct material behaviors depending on playing conditions and formats. For multi-day First-Class and Test cricket, kits demand high thermal deflection, heavy UPF 50+ ultraviolet filtering, and long-wear shape retention to withstand grueling eight-hour field sessions under tropical solar radiation. Conversely, white-ball T20 and One-Day International (ODI) cricket uniforms prioritize hydrophilic capillary moisture dispersion, hyper-vivid dye sublimation, anti-chafing mechanical stretch, and dynamic ventilation gussets located at peak perspiration zones—such as underarm armholes, inner collar bands, and lumbar panels.
When enterprise procurement directors, franchise kit managers, and sports brand owners audit cricket uniform manufacturing suppliers, evaluation hinges on five decisive engineering parameters:
A comparative structural audit evaluating production capabilities, lead times, minimum order quantities (MOQ), and specialized value propositions across top international cricket gear producers.
| Manufacturer / Supplier | Location / Hub | Core Strengths & Specialty | MOQ Flexibility | Average Lead Time | Best Suited For |
|---|---|---|---|---|---|
| Bralen Industries (Pakistan) Direct Factory OEM / ODM | Sialkot, Pakistan | In-house knit-to-finish production, high-definition sublimation, rapid 7-day proto sampling, zero-middleman pricing. | Low (10–25 pcs) | 2–4 Weeks Bulk | Global Pro Clubs, Private Label Brands, Importers & Academies |
| Kukri Sports Multinational Brand | United Kingdom | Heritage collegiate and county cricket kit supplier; robust bespoke 3D design portal. | Medium (50 pcs) | 6–8 Weeks | UK County Clubs, Independent Schools & Universities |
| Gray-Nicolls Heritage Gear Specialist | Robertsbridge, UK / Aus | Iconic cricket heritage; traditional whites and protective equipment integration. | High (100 pcs) | 8–10 Weeks | Traditional Cricket Leagues, International Boards & Retailers |
| Masuri Group Protective & Apparel | Winchester, UK | Pioneers in high-spec batting helmets; modern athletic apparel line with premium fabrics. | Medium (50 pcs) | 5–7 Weeks | Semi-Professional Clubs & County Age-Group Teams |
| TYKA Sports Subcontinent Franchise Supplier | Jalandhar, India | High-profile sponsor for IPL franchises; extensive sublimation capacity for local tournaments. | Medium (50 pcs) | 4–6 Weeks | Franchise T20 Teams & Large Academy Networks |
| Canterbury of NZ Rugby & Multi-Sport | Auckland, New Zealand | Legendary seam resilience, heavy-duty fabrications suited for rugged athletic conditions. | High (100 pcs) | 8–12 Weeks | Australasian Sports Clubs & Multi-Sport Organizations |
| Spartan Sports Commercial Equipment & Kit | Sydney, Australia | High-profile athlete endorsements; bold dynamic team kit styling and fan merchandising. | Medium (50 pcs) | 6–8 Weeks | Commercial Merchandisers & Amateur Club Tournaments |
| SS Sports (Sareen Sports) Subcontinent Powerhouse | Meerut, India | Expansive equipment catalog with expanding sublimated apparel production facilities. | Medium (50 pcs) | 4–7 Weeks | Grassroots Cricket Clubs & South Asian Distributors |
| BLK Sport Engineered Performance Kits | Gold Coast, Australia | High-tech compression panels and custom collar architecture for elite athlete fit. | High (75 pcs) | 6–9 Weeks | Elite Tier Franchises & National Governing Bodies |
| Shrey Sports Contemporary Teamwear | Delhi NCR, India | Modern slim-fit cricket cuts, lightweight sweat-wicking poly blends, fast stock distribution. | Low-Med (30 pcs) | 4–6 Weeks | Modern T20 Squads & Youth Performance Centers |
How cutting-edge yarn formulations, sustainable recycling protocols, and ergonomic pattern cutting are redefining performance expectations on the cricket pitch.
Global federations are shifting aggressively toward certified GRS (Global Recycled Standard) recycled polyester extruded from sanitized ocean-bound polyethylene bottles. These fibers match virgin polyester in tensile strength (3.8 cN/dtex) and dye affinity while slashing lifecycle carbon emissions by 42%.
Modern uniform construction blends solid 150 GSM interlock across high-wear chest and shoulder panels with hyper-porous 110 GSM micro-diamond mesh across side gussets and the lower spine. This dual-density mapping accelerates convective body heat dissipation during peak cardiovascular exertion.
Unlike topical zinc coatings that wash away after 10 cycles, next-generation cricket uniforms incorporate non-migrating organosilane antimicrobial polymers bonded directly into the yarn matrix. This inhibits odor-causing bacterial replication (Staphylococcus aureus) throughout high-humidity summer tournaments.
Traditional heavy stitched twill crests add unwanted weight and cause chest chafing under intense running. Modern franchise uniforms employ ultra-thin (180-micron) elastomeric 3D silicone transfers that offer tactile raised relief, sharp color fidelity, and frictionless comfort against bare skin.
With performance analytics now standardized across youth academies and elite national squads, cricket playing jerseys and baselayer compression vests feature integrated, zero-bounce neoprene pockets situated between the scapulae to hold high-frequency micro-GPS tracking devices securely.
Cricket uniforms designed for harsh sunshine in Australia, the Middle East, and South Asia leverage specialized sun-reflective textile treatments. These chemical finishes reflect up to 80% of heat rays from dark-colored fabrics, reducing kit surface temperatures by up to 5°C compared to untreated polyester.
How supply chain digitalization, micro-batch agile replenishment, and decentralized factory fulfillment are reshaping B2B ordering for distributors, sporting associations, and private labels.
Historically, sports distributors were forced to place mammoth bulk orders 6 to 9 months before seasonal opening fixtures, leading to severe inventory lock-up, stockouts on popular sizes (M and L), and heavy off-season discounting on unsold goods. The industry is rapidly migrating toward Agile Rapid-Response Manufacturing. Utilizing high-speed industrial dye-sublimation printers and laser fabric cutting beds, modern factories can initiate initial orders of 100 units, followed by fast-turn repeat replenishment batches of 10–25 units delivered via air express in under 12 working days.
B2B sourcing workflows have transitioned away from slow physical paper spec-sheets. Importers now deliver CLO3D or Browzwear digital garment files directly to the factory's CAD cutting station. Digital size grading algorithms instantly adjust panel proportions across youth sizes (Y-XS to Y-XL) through adult sizing (XS to 5XL) without distorting sponsor placement, sublimated side vectors, or club crest proportions. This cuts pre-production sampling iterations from three rounds down to a single golden seal confirmation sample.
With stringent global import regulations entering into force—such as the EU Corporate Sustainability Due Diligence Directive (CSDDD) and US UFLPA border audits—international apparel buyers demand complete supply chain pedigree. Suppliers must provide auditable paper trails demonstrating zero forced labor, non-toxic chemical disposal certifications (ZDHC Level 3), safe worker conditions, and certified yarn origin from accredited spinning mills.
Located in the heart of Sialkot, Pakistan—the world's historic capital for athletic equipment and teamwear craftsmanship—Bralen Industries provides end-to-end vertically integrated OEM, ODM, and private label apparel production.
By interfacing directly with our Sialkot factory cutting, printing, and sewing lines, enterprise buyers bypass European and American trading agents, saving 20–35% on landed unit costs.
Our in-house master pattern makers lock approved pre-production samples as strict golden benchmarks. Every production batch is verified against digital spec tolerances within ±0.5 cm.
From initial tech pack or vector artwork confirmation, our rapid-sampling division prepares custom lab dips, prints sublimation strike-offs, and delivers physical samples via DHL/FedEx Express.
Quality control operates continuously across 4 checkpoints: raw fabric tensile testing, inline stitching inspection, color fastness wash audits, and pre-shipment export carton checks.
We provide retail-ready private label packaging: woven damask neck labels, heat-transfer wash tags, barcoded hang tags, custom-printed matte frosted polybags, and retail display cartons tailored for brick-and-mortar sports outlets or direct Amazon FBA replenishment.
Our dedicated export customs department coordinates worldwide multimodal freight forwarding. Whether air-freighting rush orders to Heathrow, Sydney, or JFK in 4–6 business days or dispatching 20ft ocean containers to Rotterdam or Jebel Ali, we manage customs documentation end-to-end.
Managing squad uniform variations is seamless. Our automated raster image processing (RIP) software handles individual player surnames, captaincy badging, club crests, sponsor placements, and official squad numbers without incurring auxiliary tooling or screen-setup setup charges.
Comprehensive technical guidance addressing minimum orders, technical specifications, wash resilience, sizing parameters, and international export procedures.
For fully custom dye-sublimated match jerseys and trousers, our production MOQ starts at just 10 to 15 pieces per design with mixed sizing (Youth to Adult 5XL), making it ideal for amateur clubs, schools, and promotional campaigns. For complex cut-and-sew apparel featuring custom-dyed yarns, specialized jacquard collars, or heavy fleece tracksuits, our standard MOQ is typically 50 to 100 pieces per colorway.
Full-dye sublimation is the gold standard for cricket jerseys. Inks are molecularly bonded into the polyester fibers under high thermal pressure (210°C), resulting in a weightless, breathable graphic with zero hand-feel that will never crack, peel, or fade over time. Screen printing, while cost-effective for simple one-color t-shirts, creates a solid rubberized film over fabric pores that inhibits sweat evaporation and adds unnecessary weight.
To provide a firm price quotation and sampling schedule within 24 hours, our merchandising department requires: (1) Garment style or rough sketch/reference image, (2) Fabric specification or preferred GSM/weight, (3) Total estimated order quantity and size breakdown, (4) Vector artwork files (AI, EPS, PDF) with designated Pantone PMS color codes, and (5) Intended delivery destination and target in-hand date.
Yes. We regularly manufacture official First-Class and multi-day match apparel following International Cricket Council (ICC) and Marylebone Cricket Club (MCC) equipment standards. This includes exact cream/ivory shade matching, strict sizing and positioning compliance for manufacturer logos (under 100 cm²), designated collar logos, and approved chest sponsorship dimensions.
Digital 2D/3D mockups are generated within 24–48 hours. Physical proto-samples require 7 to 12 working days. Once the golden sample is approved and bulk fabric booking is initialized, bulk manufacturing takes between 3 to 5 weeks depending on batch size. Courier air shipping via DHL Express takes 4–6 business days globally, while ocean container shipping takes 22–32 days depending on the port of discharge.
We log every client's digital sublimation profile, ICC color curves, and specific Pantone PMS color codes in our computerized production archives. When a club reorders kits six or twelve months later, the exact same disperse ink formulation, transfer temperature, and dwell timing are loaded, guaranteeing a 99.5% visual shade match between existing player uniforms and incoming replenishment stock.
Speak directly with our senior athletic textile engineers. Whether you require 25 custom franchise team kits or 10,000 retail-ready private label polo shirts, we deliver premium sports manufacturing excellence on schedule, every single season.
