
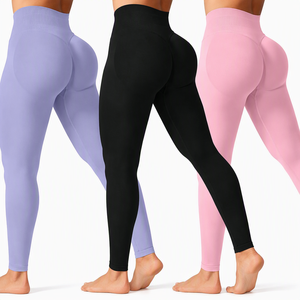
Seamless Athletic
Direct factory-floor manufacturing samples reflecting our four-way tensile resilience, moisture-management capillary action, and high-density technical stitch standards.
Evaluated according to ISO 9001 adherence, tackle twill machine gauge tolerances, sublimation ink migration mitigation, and supply-chain transparency.
Renowned for full vertical integration in Sialkot, Bralen Industries leads the sports apparel manufacturing ecosystem. Providing true OEM/ODM full-package manufacturing, their facility houses in-house flat-lock stitching stations, multi-head tackle twill embroidery systems, and Japanese sublimation presses. Ideal for brand labels, collegiate athletic departments, and retail-grade street-fashion jerseys looking for custom-dyed fabrics and rapid sampling.
An industrial powerhouse serving massive global volume contracts. Tondu excels at high-speed sublimation output utilizing Italian Kiian inks on synthetic lightweight polyester fabrics. Suitable for distributors managing corporate promo jerseys and multi-thousand high school athletic programs where unit cost optimization dominates decision parameters.
A baseline cornerstone for North American domestic decorators. Augusta holds vast domestic warehouse inventories of blank button-down and two-button baseball jerseys. While customization happens downstream, their turn-times on unprinted blanks are unbeatable for fast in-season roster fill-ins.
Capitalizing on USMCA zero-tariff corridors, this facility supplies Mid-Atlantic and Southern US markets with short overland logistics cycles. They specialize in double-knit warp-knitted traditional baseball vests and button-downs with standard twill appliques.
Historically holding the gold standard for MLB on-field performance patterns, the institutional wholesale division continues to supply collegiate, minor league, and high-spec club clients. Pricing commands a premium due to strict license-grade patterning tolerances.
Specialized engineering in engineered-ventilation fabrics. Boost Textile builds custom engineered bird-eye and pinhole micro-mesh baseball jerseys with laser-cut ventilation underarm gussets designed specifically for hot-weather leagues.
Providing pan-European delivery for European baseball federations and fashion micro-labels. Viking Pro relies heavily on OEKO-TEX Standard 100 certified recycled yarn systems, offering high environmental compliance documentation.
Positioned closely to Southern Asian raw cotton and synthetic extrusion spinning mills, this factory delivers budget-optimized team packages including matching pants and socks alongside classic full-button baseball tops.
A boutique cut-and-sew domestic shop providing rush turnarounds (7-10 days) on sewn lettering and retro wool-blend vintage replica jerseys. Best leveraged for short-run commercial promotions and entertainment production requirements.
Bridging the gap between on-field athletic cut jerseys and contemporary oversized streetwear apparel lines. StitchCraft specializes in heavy-duty 280 GSM polyester mesh, premium metal snap closures, direct embroidery chest badges, and private-label fashion packaging.
Understand the tensile strength, air permeability, and weight tradeoffs before issuing procurement tenders.
| Fabric Classification | Composition & Weight | Primary Utility | Mechanical Durability | Recommended Decoration Method |
|---|---|---|---|---|
| Pro-Weight Double Knit | 100% Polyester / 220-250 GSM | Traditional on-field, pro-tier club wear | Exceptional resistance to sliding abrasions | Multi-Layer Tackle Twill, Direct Chenille Embroidery |
| Aerated Pin-Hole Mesh | 92% Poly, 8% Spandex / 160-180 GSM | Summer leagues, warm-climate tournaments | High flex elasticity; moderate abrasion wear | All-Over Dye Sublimation, Heat Seal Silicone |
| Warp-Knit Interlock | 100% Micro-Poly / 140-160 GSM | Youth leagues, promotional jerseys, fan apparel | Ultra-light hand feel; prone to snagging if unbrushed | Full Dye Sublimation, Screen Print Inks |
| Vintage Wool-Flannel Blend | 60% Wool, 40% Poly / 300-340 GSM | Heritage collections, street fashion labels | High thermal mass, premium heritage feel | Felt Applique, Direct High-Density Embroidery |
How changing international trade restrictions, environmental legislation, and fashion trends reshape the baseball jersey wholesale pipeline.
Baseball jerseys have largely migrated outside the diamond into lifestyle apparel. Demand is shifting away from thin 120 GSM jerseys toward luxury 240+ GSM weights with custom engraved corozo buttons, boxy dropshoulder profiles, and heavyweight interior neck tapings tailored for streetwear brand drops.
European and North American institutional procurement guidelines now routinely specify GRS (Global Recycled Standard) certification. Top tier mills are dropping virgin polyester chips in favor of post-consumer plastic bottle flake extrusions without sacrificing tensile slide durability.
Pure tackle twill has high sewing labor costs, while pure dye sublimation lacks dimensional luxury. The emerging procurement compromise is sublimated laser-cut twill cresting—sewn via computerized programmable zigzag stitch machines to yield dimension while allowing complex gradient artwork.
Eliminating intermediaries through true factory-floor ownership based in the world's premier sports goods manufacturing cluster.
Operated entirely in-house without domestic brokerage agents. Our clients interact directly with production pattern makers and senior sample technicians, preserving clear tech-pack translations and uninflated pricing models.
Every signed sample is officially sealed with detailed measurement records across 18 separate garment points. Bulk assembly must test inside a strict ±1.0cm tolerance before shipping boxes are sealed for export.
From dye-sublimated neck labels to silicone heat transfers, woven side-seam flag labels, hang tags with custom SKU barcodes, and individual polybags compliant with Amazon FBA fulfillment rules.
Get immediate clarity on trade finance terms, minimum order thresholds, and technical artwork requirements.
For full-dye sublimation orders, our baseline MOQ typically starts at 20-30 pieces per design, allowing custom rosters, names, and numbers. For complex cut-and-sew orders demanding custom-milled or custom-dyed pantone fabrics and heavy multi-layer tackle twill embroideries, baseline MOQs typically sit between 100 to 200 units per style run.
Dye migration (disperse dye bleeding into embroidery threads or twill fabric) is avoided by using high-grade bleeding-block barrier underlays, thermo-stable twill twines, and strict dye bath fixation temperatures above 135°C during raw synthetic textile dyeing runs.
Physical pre-production counter-samples are generally completed and couriered via DHL/FedEx in 7 to 14 business days from technical spec sign-off. Bulk commercial container and air shipments generally require 3 to 5 weeks depending on embroidery complexity and total garment quantities.
Supplying a technical specification pack containing fabric GSM, target composition, size breakdown matrix, vector artwork (Adobe Illustrator .AI or vector .PDF format with fonts converted to outlines), and exact Pantone color codes allows our merchandising division to deliver a confirmed FOB or DDP quotation within 24 hours.
Whether you are developing an athletic team roster program or an upscale cut-and-sew streetwear collection, our engineering team in Sialkot provides end-to-end guidance from tech pack development to international logistics.
Send an Inquiry