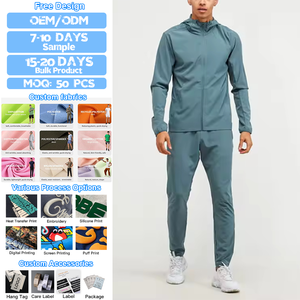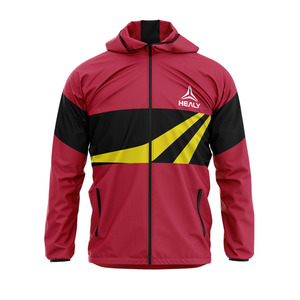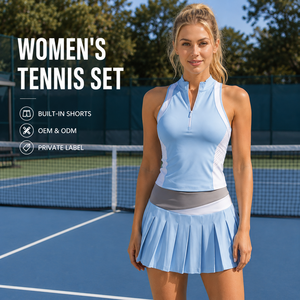
Every apparel silhouette below is engineered in-house from spec to export carton. Designed for extreme durability, high-tensile sports court training, and rigorous institutional athletic programs.
Situated in Sialkot, Pakistan—the epicenter of FIFA-grade soccer production and international athletic apparel exports—our facility pairs time-tested textile master craftsmanship with cutting-edge Japanese dye-sublimation and German laser cutting hardware.
We eliminate supply chain latency through complete in-house operations. From fabric knits inspection and computerized pattern grading to wide-format dye sublimation, precision sewing, multi-point QC, and direct export cartoning, everything remains strictly under our technical custody.
Our digital printing utilizes certified Italian Kiian and J-Teck disperse dyes transferred at 205°C via Monti Antonio calenders. This molecular dye-gasification process yields Oeko-Tex Standard 100 Class I certified garments with zero cracking, peeling, or breathability loss across 100+ commercial wash cycles.
By bypassing overseas brokers and third-party trading agents, purchasing directors secure tier-1 factory pricing directly from our Punjab manufacturing floor. This transparent framework enables razor-sharp landed costing, dynamic volume breaks, and agile production line scheduling.
Selecting the ideal manufacturing methodology determines structural longevity, thermal comfort, unit economics, and minimum production runs. Evaluate our production pathways below.
| Manufacturing Technique | Optimal Athletic Applications | Core Technical Advantages | Material Constraints | Typical Volume MOQs |
|---|---|---|---|---|
| Full All-Over Dye Sublimation | Soccer Kits, Basketball Uniforms, Rugby Jerseys, Cycling Jerseys, Esports Teamwear | Zero hand-feel; unlimited chromatic gradients; uncompromised fabric micropores; permanent thermal bonding. | Requires polyester-dominant blends (>85% PET composition) for optimal sublimation color saturation. | Low-to-Flexible (10 - 25 units per roster design) |
| Cut & Sew Engineered Panels | Gym Tracksuits, Training Hoodies, Compression Pants, Outerwear Jackets | Dynamic tactile texture; integration of engineered jacquard ventilation meshes; premium mixed-media aesthetics. | Higher tooling and precision knife setup; pattern grading complexity increases with intricate paneling. | Medium (100 - 250 units per colorway) |
| Direct-to-Film (DTF) & Silicone 3D | Club Crest Badging, Sponsor Logos, High-Density Emblems, Outerwear Accents | Hyper-sharp vector edge fidelity; dimensional tactile height (0.5mm - 1.2mm); elastomeric multi-directional stretch. | Requires strict calender temperature profiling (±2°C) to prevent synthetic fabric heat-burn marks. | Flexible (50 units per design program) |
| Tackle Twill & Heavy Embroidery | Varsity Team Jackets, Traditional Baseball Uniforms, Ice Hockey Sweaters | Classic institutional aesthetic; exceptional abrasion resistance; high perceived retail and league value. | Adds localized physical weight; not recommended for lightweight high-velocity endurance fabrics (<140 GSM). | Medium (50 - 100 units per style) |
Need custom engineered fabric weights or specialized knit blends? Our R&D lab will knit and test custom yarn compositions according to your tech pack parameters.
International sourcing directors and institutional team apparel distributors face rapid structural shifts. Align your procurement pipeline with these four transformative commercial developments.
Global athletic governing bodies increasingly mandate recycled performance polymers. Forward-thinking procurement plans now prioritize certified GRS (Global Recycled Standard) recycled polyester (rPET) derived from post-consumer PET bottles. Our Sialkot mill provides virgin-equivalent tensile strength and color clarity while reducing lifecycle carbon footprints by up to 45% compared to petrochemical polyester.
The era of holding 10,000 seasonal units of static inventory is being replaced by agile, responsive supply chains. Importers now establish rolling baseline purchase orders paired with 7-to-14 day replenishment cadences. Our digital sublimation pipeline lets brands launch localized team rosters and special tournament kits without incurring deadstock risks or write-offs.
Pre-production sampling cycles have dropped from 4 weeks to under 48 hours via CLO3D, Browzwear, and computerized 2D-to-3D tension simulations. We generate photorealistic rendering maps that allow institutional buyers to approve grading, seam line transitions, and sponsor positions before running physical fabric through our automated Gerber cutters.
Sportswear structural failure on match day destroys brand credibility. Our plant enforces a zero-defect quality architecture based on internationally recognized ANSI/ASQ Z1.4 (ISO 2859-1) Level II AQL standards.
Every imported and circular-knitted textile roll undergoes automated inspection under high-CRI light tables. We eliminate yarn slubs, shade variation across rolls, elastane unevenness, and chemical moisture irregularities prior to cutting.
Using digital X-Rite spectrophotometers, our dye chemists calculate chromatic variance against client-specified Pantone TPX/PMS codes. We hold bulk dye-sublimation runs to a tight tolerance of ΔE < 0.8, guaranteeing flawless kit uniformity across multi-season releases.
Finished samples undergo seam burst testing, hydro-abrasion rub cycles, and repeated 60°C industrial laundering simulations. We guarantee that all flatlock stitches, silicone prints, and heat-welded pockets maintain tensile integrity without delamination.
Authoritative answers to the commercial, logistical, and technical questions most commonly submitted by brand buyers, retail chains, and international athletic federations.
For full-dye sublimated performance teamwear (soccer, basketball, rugby, track), our baseline MOQ starts as low as 10 to 20 units per design with mixed player sizing and roster names/numbers. For custom-milled, piece-dyed cut-and-sew fabrics or seamless compression lines, MOQs typically range from 100 to 200 units per colorway due to knitting machinery setup parameters.
We utilize dedicated RIP color calibration profiles tuned specifically to our Japanese dual-head printers and Italian disperse inks. Clients supply Pantone Solid Coated (PMS) or TPX codes; we print strike-offs on the exact target polyester substrate and review them under standard D65 daylight boxes before running production orders.
Physical pre-production counter-samples are produced and ready for courier dispatch within 7 to 10 working days following digital tech pack approval. Bulk production for orders ranging from 500 to 10,000 units averages 3 to 5 weeks, followed by express air cargo (3-5 days delivery) or consolidated ocean freight (20-30 days).
Yes. We deliver 100% retail-ready apparel. Our services include high-definition woven or heat-transfer brand neck labels, multilingual care tags, FSC-certified hang tags with scannable EAN/UPC barcodes, customized frosted zip-seal polybags, and heavy-duty 5-ply export master cartons ready for direct fulfillment or Amazon FBA intake.
We commonly contract under FOB (Karachi or Sialkot Dry Port), CIF, and DDP (Delivered Duty Paid) terms. For European, North American, and Australian buyers seeking seamless logistics, our forwarding desk handles all export documentation, customs clearances, tariff filings, and inland trucking directly to your warehouse.
Confidentiality is an essential pillar of our industrial service. We execute formal bilingual Non-Disclosure Agreements (NDAs) prior to receiving client tech packs or vector art. Your proprietary patterns, tournament assets, brand colorways, and artwork files are stored on isolated, secure servers and will never be shared or displayed without permission.
Partner directly with an established Sialkot OEM/ODM manufacturer. Submit your tech pack, vector concepts, or uniform tender specifications to receive an engineered cost breakdown and production schedule within 24 business hours.