
Compression Line
Manufactured to international sporting federation tolerances. Available for direct OEM cut-and-sew customization, sub-micro sublimation printing, and private-label packaging.
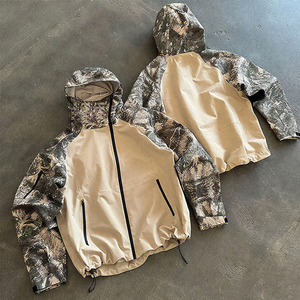

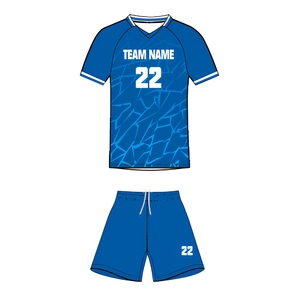
Rugby demands garment durability beyond standard football or athletic apparel. From rucks and scrums to open-field tackles, a match-grade jersey must withstand multiaxial tensile loads exceeding 650 Newtons without structural failure.
Modern professional rugby uniforms utilize circular-knitted and warp-knitted polyester blends combined with 8% to 14% high-modulus elastane. Fabric density ranges strictly from 280 GSM to 340 GSM for match front-rows, and 240 GSM to 270 GSM for backline positions.
Seam failure is the primary cause of discarded kits in contact leagues. Our manufacturing facility employs four-needle six-thread (flatlock) ISO 607 stitching paired with computerized bar-tacking along every high-stress kinetic junction point.
We utilize industrial Italian thermal sublimation presses operating at 210°C, infusing non-toxic azo-free dye particles directly into the polymer core. This ensures breathability remains 100% unimpeded across intense physical combat.
Choosing the right technical specification aligns cost per unit with commercial objectives. The matrix below contrasts engineering tolerances across club procurement tiers.
| Performance Tier | Material Composition | Fabric Weight (GSM) | Stitching Construction | Elastane Content | Ball Grip Add-ons | Target Lifespan |
|---|---|---|---|---|---|---|
| Tier 1: Elite Pro Match | 100% High-Tenacity Poly/Spandex Interlock | 280 - 320 GSM | Flatlock 6-Thread + Double Bar-Tack | 10% - 14% Spandex | Custom 3D Silicone Dots | Multiple Full-Contact Seasons |
| Tier 2: Semi-Pro / Club Match | Moisture-Wicking Hydrofil Poly Matrix | 260 - 280 GSM | Reinforced 5-Thread Overlock + Taping | 6% - 8% Spandex | Optional Laser Texturing | 1 - 2 Full-Contact Seasons |
| Tier 3: Training & Academy | Circular Birdseye Breathable Poly Mesh | 220 - 250 GSM | Industrial Overlock with Safety Stitch | 4% - 6% Elastane | None | High-Frequency Daily Drills |
| Tier 4: Supporter & Commercial | Lightweight Poly Pique or Double-Knit | 160 - 200 GSM | Standard Chainstitch with Clean Finish | 0% - 3% Stretch Poly | None | Retail Lifestyle Wear |
Supply chain executives and kit procurement managers are restructuring their vendor portfolios around four macroeconomic shifts in performance apparel manufacturing.
Tender frameworks across European and Commonwealth rugby unions now mandate a minimum of 65% to 100% GRS (Global Recycled Standard) post-consumer poly. Next-generation rPET yarns match virgin polymers in bursting strength while reducing upstream manufacturing carbon emissions by 42%.
Physical sampling waste is diminishing via 3D virtual garment modeling (CLO3D). Importers validate grading from Youth XS to Men's 6XL digitally, allowing zero-latency pattern approval, cutting fabric consumption loss down to under 5% through AI nesting algorithms.
Tier 1 & Tier 2 rugby squads now require seamless encapsulated pockets between shoulder blades to house Catapult and STATSports GNSS tracking monitors. Seams must be hydro-bonded to prevent device chafing against the thoracic spine during high-impact tackles.
Inventory holding costs have catalyzed a shift from massive singular container drops to scheduled seasonal micro-batches. Factories equipped with agile direct-to-textile sublimation and modular sewing cells allow clubs to top up roster kits within 10 to 14 business days.
Sialkot, Pakistan produces the world's most demanding athletic gear, including official tournament match balls and elite rugby sportswear. Our facility channels this century-old industrial heritage into a tightly monitored, socially compliant export infrastructure.
Procuring through European or Australian trading companies adds 35% to 50% in markups. Working directly with our Sialkot manufacturing floor gives you transparent BOM (Bill of Materials) visibility, custom fabric milling access, and unmatched cost-performance metrics.
From raw greige fabric inspection to color spectrometry, dimensional stability testing after 5 industrial wash cycles, tensile yield testing, and final carton drop audits, every production batch is governed by dedicated in-line QA auditors prior to dispatch.
We handle end-to-end freight documentation: FOB Karachi, CIF Felixstowe/Rotterdam/Long Beach, or DDP direct to your commercial distribution warehouse. Full GSP certification support ensures preferential tariff clearance in the EU, UK, US, and Oceanic jurisdictions.
Direct answers addressing Minimum Order Quantities (MOQs), technical development timelines, fabric certifications, private-label branding, and international freight delivery terms.
For fully customized sublimation rugby match jerseys, our baseline MOQ begins at 25 units per design, accommodating full player size assortments (XS to 5XL) and individual player names/numbers. For custom-dyed cut-and-sew apparel utilizing specialized knit pantones, the MOQ is 200 units per colorway.
Physical fit and proto samples are produced and air-couriered within 7 to 10 working days. Following sign-off of the "golden sample," bulk production generally requires 3 to 4 weeks depending on order scale. Express air freight takes 4 to 6 business days, while consolidated sea shipping requires 22 to 32 days depending on destination port.
Yes. We strictly fabricate match uniforms, padded base-layers, and technical headgear in compliance with World Rugby Regulation 12 specifications. This covers seam tensile security, maximum allowable padding thickness/density (cellular foam <= 10mm thickness and density <= 45kg/m³), and the total exclusion of metallic hardware or rigid protrusions.
For OEM contracts, an Adobe Illustrator (.AI) or vector PDF tech pack specifying measurement grade charts, Pantone TPX/TCX color codes, placement measurements, and trim specs is ideal. For ODM clients, reference garments, physical samples, or design sketches with desired fabric GSM are sufficient for our in-house CAD department to engineer a full pattern specification sheet.
We supply fully integrated retail packaging: satin or heat-sealed branded inner neck labels, FSC-certified hangtags with scannable EAN/UPC barcodes, customized polybags with safety ventilation holes, and master cartons with custom shipping marks formatted for third-party logistics fulfillment centers (e.g., Amazon FBA, DHL Supply Chain).
Our dye laboratory relies on Datacolor spectrophotometer analysis calibrated against the universal Pantone Solid Coated / Textile system. Digital proof profiles are locked and archived inside our Italian sublimation software. Every production run undergoes side-by-side swatch evaluation under D65 artificial daylight booths to ensure delta-E variances remain below 1.0.
Partner directly with an established Sialkot manufacturing authority. Contact our technical apparel merchandising team today to discuss fabric weights, custom pattern development, rapid sample delivery, and institutional volume tier pricing.