Precision-engineered fitness garments built with performance-grade four-way stretch, sweat-wicking synthetic matrixes, and multi-needle reinforced ergonomics.
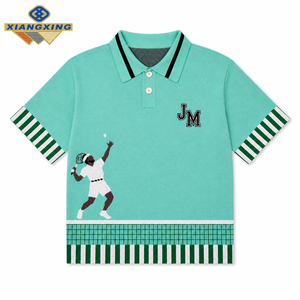
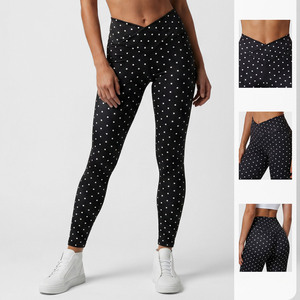
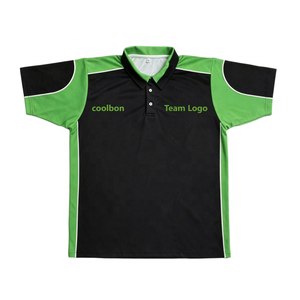
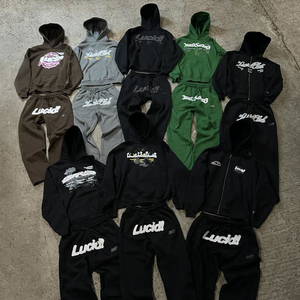
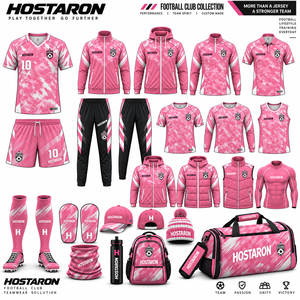
A strategic breakdown of how Tier-1 China contract manufacturers utilize end-to-end fabric development, precision automation, and circular logistics to outperform conventional athletic garment sourcing.
The global workout apparel landscape has transformed from basic aesthetic athleisure into highly engineered ergonomic equipment. Today's commercial fitness consumer demands compression garments that provide targeted muscle stabilization, moisture-wicking base layers that regulate microclimate temperatures, and high-impact sports bras that offer mechanical support without causing cutaneous abrasion. For direct-to-consumer (D2C) brands, international sports clubs, and athletic distributors, choosing the right China wholesale custom workout clothes manufacturer is the decisive variable between high return rates and scalable brand loyalty.
In China’s primary textile hubs—spanning Guangdong, Zhejiang, and Fujian—the sportswear production ecosystem is distinguished by its upstream industrial cluster density. Unlike regional assembly operations that rely on imported synthetics, our integrated manufacturing model controls the lifecycle from filament polymer extrusion and circular knitting to digital dye sublimation, laser pattern cutting, automated sewing, and stringently monitored cleanroom packaging. This end-to-end supply chain integration compresses sampling cycles to under ten days and provides robust traceability for technical certifications including OEKO-TEX Standard 100, Global Recycled Standard (GRS), and ISO 9001 compliance.
How institutional sportswear buyers are re-engineering their procurement playbooks to mitigate inventory risk, navigate trade logistics, and capitalize on digital manufacturing.
Traditional multi-round physical prototyping creates significant material waste and prolongs design cycles by weeks. Enterprise procurement protocols are transitioning to 3D computer-aided pattern modeling (such as CLO3D and Browzwear).
The era of rigid 5,000-piece single-color minimums is being replaced by responsive supply contracts. Brands mitigate inventory risk by testing new drops with agile minimum order runs before committing to deep inventory.
Stricter cross-border regulations (such as the EU Corporate Sustainability Due Diligence Directive) require full supply chain visibility from raw resin to packaged garment.
An in-depth analysis of high-performance textile constructions, bonding chemistries, and ergonomic stitch geometry reshaping the activewear sector.
By deploying high-diameter Santoni seamless circular knitting machinery, we produce engineered gradient compression zones directly into the fabric tube. This removes lateral seams, elevates tensile durability, and prevents chafing during repetitive, high-impact athletic movements.
For elite running and cycling collections, thread stitching is increasingly supplemented by ultrasonic cutting and thermoplastic polyurethane (TPU) bonding films. This creates featherweight, flat-profile joints that minimize skin drag while withstanding repeated wash delamination testing.
Modern moisture management avoids temporary surface-applied chemical dips. We utilize dual-surface knitting techniques pairing hydrophilic inner micro-polyester with moisture-dispersing outer nylon, pulling sweat away from the dermis via capillary pressure.
| Fabric Classification | Composition Ratio | Areal Density (GSM) | Recommended Category | Technical Features |
|---|---|---|---|---|
| Bare-Feel Interlock | 75% Nylon, 25% Spandex | 220–240 GSM | Yoga Leggings, Soft Bras | Brushed Peach Finish Squat-proof opacity, 4-way mechanical stretch |
| Aerodynamic Poly-Mesh | 92% Recycled Poly, 8% Elastane | 110–130 GSM | Pro Cycling, Marathon Tees | Hexagonal Vent Hole Drag reduction, rapid moisture vapor dispersion |
| Hydro-Compression Knit | 78% Polyamide, 22% Elastane | 260–290 GSM | Recovery Tights, Base Layers | Graduated Compression Muscle oscillation dampening, UV UPF 50+ |
| Heavyweight French Terry | 80% Combed Cotton, 20% Poly | 380–420 GSM | Athletic Hoodies, Joggers | Loopback Thermal Zero-shrinkage wash, dense hand-feel, anti-pilling |
| Diamond Ripstop Microfiber | 100% Interlock Polyester | 140–160 GSM | Soccer Kits, Basketball Uniforms | Sublimation Ready High burst strength, snag-resistant woven structure |
Combining industrial scale with tailored craftsmanship: Discover how our production floor ensures technical accuracy across every phase of production.
By housing computerized fabric spreading, precision laser pattern grading, clean-room dye sublimation, flatlock stitching lines, and finished packing in a centralized facility, we eliminate subcontractor markups, cut communication latency, and protect your intellectual property.
Quality control is embedded into every operational step rather than treated as a post-facto sorting process. Our certified QC technicians perform 4-point fabric roll inspections, inline sewing tension monitoring, dry and wet rub fastness assessments, and final dimensional tolerance audits against your approved tech pack.
We deliver store-ready, shelf-compliant merchandise designed to elevate your brand perception. We provide custom-molded silicone badges, ultra-soft tagless neck transfers, custom branded drawstrings, embossed aglets, barcoded biodegradable polybags, and retail master cartons packed to Amazon FBA or third-party logistics (3PL) specs.
Essential guidance covering technical specifications, sampling turnaround, minimum order volumes, and international customs clearance.
