
Windbreaker Tech
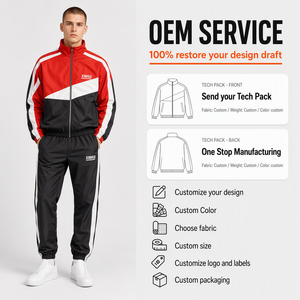
Engineered for endurance sports, lifestyle athleisure, and professional club performance. Every product line is fully customizable across GSM weight, fit grade, pocket geometry, and embellishment protocols.
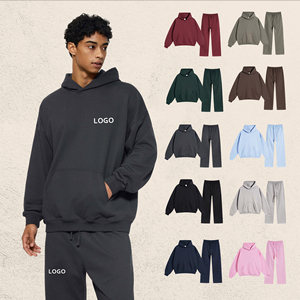
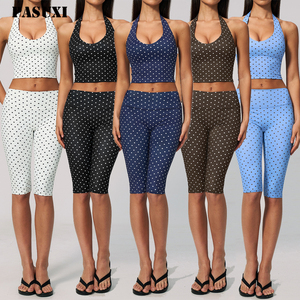
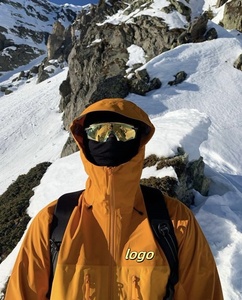
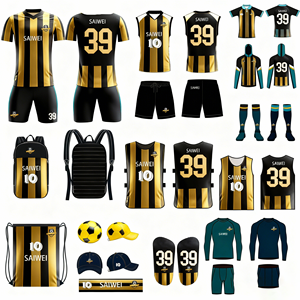
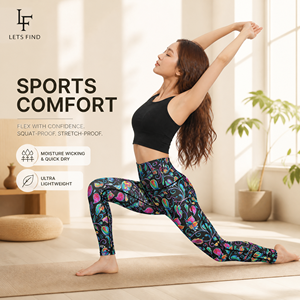
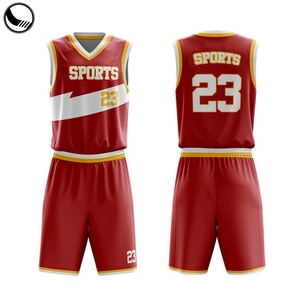
As premier Chinese suppliers and global exporters of high-performance track pants and athletic sweatsuits, our production methodology moves beyond conventional cut-and-sew operations. We operate a tightly controlled technical apparel development framework engineered around yarn morphology, seam durability, and multi-directional kinetic recovery.
Commercial activewear programs demand strict adherence to tensile integrity and shrinkage control. Whether producing 430 GSM heavyweight casual loungewear or lightweight crinkle nylon windbreaker joggers, our technical design department integrates localized reinforcement at high-stress pivot zones—specifically the crotch junction, inner thigh abrasion zones, and pocket entrance corners.
| Performance Fabric | Composition & Weight | Key Mechanical Metrics | Ideal Application |
|---|---|---|---|
| Heavyweight French Terry | 100% Combed Cotton, 420–450 GSM | Pre-shrunk, <3% dimensional change, zero pilling surface | Luxury Streetwear Bottoms & Casual Hoodies |
| Technical Stretch Tricot | 88% Polyester, 12% Spandex, 240 GSM | 4-way recovery >92%, moisture wicking <2 sec pickup | Track & Field Pants, Team Travel Warmups |
| Micro-Crinkle Ripstop Nylon | 100% Polyamide 6.6, 115 GSM | DWR C6 Coating, hydrostatic head >2000mm, tear >18N | Retro Windbreakers & Outdoor Joggers |
| Circular Seamless Compression | 75% Polyamide, 25% Elastane, 280 GSM | Graduated zoned support, high opacity, squat-proof | Performance Yoga Bottoms & Active Leggings |
To eliminate seam failure during repetitive movement, our manufacturing floors utilize calibrated differential-feed 4-needle 6-thread flatlock machinery and specialized safety-stitch overlock assemblies. High-stress zipper entries utilize ultrasonic perimeter welding or Bartack bar-tacking (28 to 42 stitches per bar), safeguarding the garment from stress shear during extreme athletic conditioning.
Critical macro shifts in raw material compliance, circular economy mandates, and near-line digital sampling protocols every international buyer must integrate into their upcoming procurement cycles.
Procurement teams are shifting rapidly from virgin synthetic blends toward chemically recycled nylon 6 (ECONYL® equivalents) and GRS-certified ocean-bound recycled polyester. Brand owners require certified chain-of-custody documentation (TC transactions) from spinning mills to port-of-loading to comply with incoming European Digital Product Passport regulations.
The traditional 6-month indent model is giving way to responsive agile replenishment. Forward-thinking brands maintain core greige yardage in our domestic warehouses, executing dye-lot call-offs or piece-dye runs in smaller batches of 300 to 500 units. This slashes terminal inventory overhang while preserving aggressive volume costing tiers.
Regulatory bans on per- and polyfluoroalkyl substances across North America and the EU require all technical windbreakers and weather-shield tracksuits to utilize advanced fluorine-free C0 durable water repellent finishes, paired with eco-friendly water-borne polyurethane backer membranes.
Combining domestic raw material supremacy with end-to-end industrial manufacturing controls, our integrated production ecosystem delivers tangible competitive advantages for global brand developers, club distributors, and enterprise activewear importers.
We operate precision 8-head Tajima embroidery machines and high-output Japanese dye-sublimation print heads with pure disperse dyes, achieving crisp vector definition without thermal bleeding or fabric stiffness.
Fabric rolls undergo 4-point inspection prior to cutting. Stitching lines are monitored continuously for needle chew, skipped stitches, and dimensional deviation against the approved master spec sheet.
From woven damask neck labels and soft silicone zipper pullers to FSC-certified custom swing tags, barcoded individual polybags, and Amazon FBA-compliant export master cartons.
Technical answers addressing minimum order volumes, laboratory sampling protocols, yarn lab-dips, and logistical handover milestones.
Our minimum order framework is structured around the chosen fabric substrate and dye technique:
Proto-samples and fit development pieces are typically dispatched within 7 to 14 business days following CAD pattern sign-off and lab-dip swatch confirmation. Mass bulk manufacturing requires approximately 3 to 5 weeks from pre-production (PP) golden sample approval, subject to order volume and embellishment complexity.
Yes. Through our specialized ODM engineering unit, our pattern makers can reconstruct complete measurement specifications, grading tables, and component bill-of-materials (BOM) from clear reference photos, benchmark physical samples, or rough technical sketches. We will produce a fit proto to verify silhouette balance before locking the master production file.
All raw fabric lots undergo spectrophotometric color evaluation under standardized D65 lighting booths. We maintain sealed master yardage swatches from approved initial dye lots. Re-orders must conform within a strict Delta E < 0.8 tolerance before passing to the computer-aided automatic nesting and cutting tables.
We support standard Incoterms including FOB (Shanghai/Ningbo/Shenzhen), CIF, and turnkey DDP (Delivered Duty Paid) via sea container or air courier. All export documentation—customs declarations, commercial invoices, bill of lading, and preferential certificates of origin—is managed by our dedicated international trade department.
Consult with our technical apparel merchandising team today. Share your design files, target GSM, and annual forecast to receive an itemized costing breakdown and sample production slot within 24 business hours.