
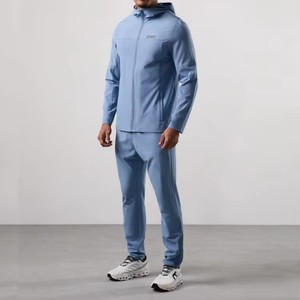
Custom Windbreaker Tracksuit For Men Set Lightweight Waterproof Outfits
- Hydrophobic micro-ripstop shell
- Ergonomic articulated knee tailoring
Direct factory production engineered to rigorous international mechanical, physical, and chemical compliance standards.
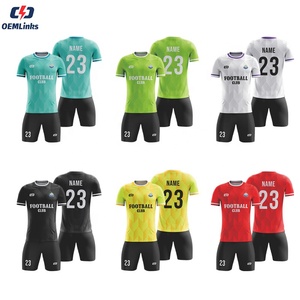
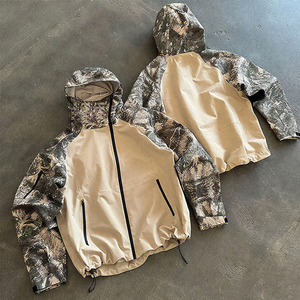
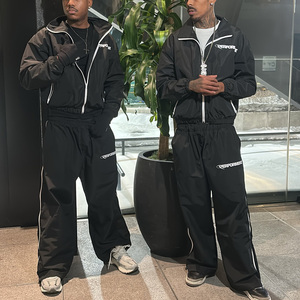
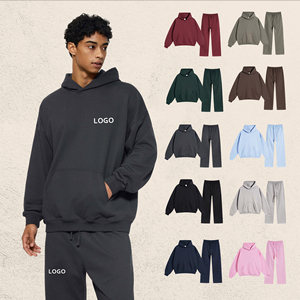
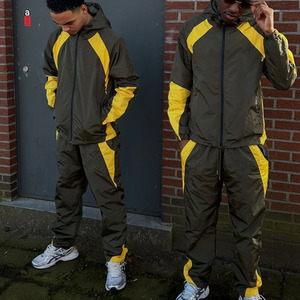
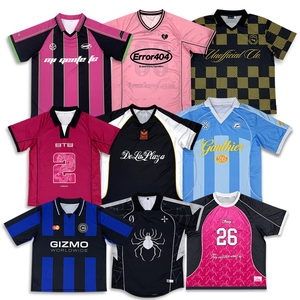
Understanding the rigorous legal, mechanical, and toxicological thresholds governing athletic team uniforms supplied to European and North American institutional markets.
In commercial teamwear procurement, navigating global conformity requires far more than aesthetic embellishment. Under European Union directives—most notably PPE Regulation (EU) 2016/425 and textile consumer directives—athletic uniforms engineered for competitive contact sports, outdoor exposure, and professional training must conform to strict physical resilience, non-toxicity, and dimensional stability metrics. As a verified OEM/ODM enterprise originating from the world’s premier sporting goods cluster in Sialkot, Pakistan, our manufacturing systems bridge the gap between bespoke agility and audited industrial compliance.
| Regulatory Standard | Test Scope & Target Category | Technical Threshold | Compliance Verification |
|---|---|---|---|
| PPE Regulation (EU) 2016/425 (Category I / Low Risk) |
Athletic outerwear, windbreakers, training jackets, weather-protective teamwear | EN 343: Resistance to water penetration (>13,000 Pa) & water vapour resistance (Ret < 20 m²·Pa/W) | Mandatory CE Mark |
| EN 17353:2020 (Enhanced Visibility Equipment) |
High-visibility training vests, nocturnal track suits, cycling and road running jerseys | Photometric performance of retroreflective tapes; chromaticity coordinates under daylight & artificial illumination | Type B2 / Type AB |
| REACH Annex XVII (EC Regulation No 1907/2006) |
All sublimated and yarn-dyed fabrics, thermal transfer films, and screen-printed inks | Zero banned azo colorants (cleavage to aromatic amines <30 mg/kg), total lead <500 ppm, non-detectable phthalates | OEKO-TEX Standard 100 |
| ISO 13934-1 / ISO 13937-2 (Mechanical Durability) |
Rugby kits, football kits, combat apparel, elastic activewear | Tensile breaking force (>350 N warp/weft), tear force (>25 N), seam slippage resistance (<2 mm displacement at 100 N) | In-House Tensometer Audit |
| ISO 105-C06 / E04 (Colorfastness Performance) |
Full dye-sublimation jerseys, printed polyamides, contrast piping | Grade 4-5 chromatic change after 50 intensive industrial laundering cycles at 60°C; resistance to acidic & alkaline perspiration | Spectrophotometer Tested |
To maintain CE certified pedigree, our vertical manufacturing ecosystem applies end-to-end batch traceability. Starting from certified OEKO-TEX Standard 100 Class II virgin or rPET yarns, every lot undergoes micro-spectroscopy to ensure the absence of carcinogenic arylamines, per- and polyfluoroalkyl substances (PFAS), and toxic plasticizers. Seam ruptures are mitigated using automated lockstitch and five-thread overlock configurations from computerized Juki and Brother automated sewing modules, ensuring that high-strain junctions withstand the aggressive shear pressures of collegiate and professional sports.
How institutional sports clubs, distributors, and global activewear brands are recalibrating their supply chain pipelines for maximum agility and ESG compliance.
Global athletic federations are enforcing strict quotas on virgin polyester. Modern procurement mandates post-consumer recycled ocean waste polyethylene terephthalate (rPET) certified under the Global Recycled Standard (GRS), reducing carbon footprints by up to 53% without sacrificing tensile elasticity or capillary wicking performance.
Physical sample rounds are being truncated from months to days via CLO3D and Browzwear parametric draping. B2B buyers now approve virtual golden samples with accurate tension mapping, reducing fabric sampling scrap by 85% and significantly shortening production lead windows for mid-season replenishable team kits.
Driven by incoming EU Ecodesign for Sustainable Products Regulations (ESPR), procurement directors are requesting integrated QR codes and woven NFC chips detailing fiber composition, country of assembly, wash protocols, and end-of-life recycling pathways directly on teamwear uniforms and tracksuits.
Supply chain shocks have made agile manufacturing clusters essential. Sialkot combines full vertical capacity—from knitting and yarn spinning to digital sublimation and cut-and-sew—allowing European and American buyers to achieve competitive FOB unit economics alongside rigorous CE and ISO quality oversight.
The convergence of functional teamwear and street fashion has altered silhouette requirements. Clubs demand boxy-fit soccer tops, heavyweight 400+ GSM French terry sweatsets, and seamless squat-proof athleisure that transition effortlessly from match competition to lifestyle retail storefronts.
Combining generations of craft heritage with audited ISO 9001:2015 precision manufacturing.
No intermediaries, broker commissions, or outsourced production confusion. We manage raw fabric procurement, yarn testing, digital transfer sublimation, laser cutting, skilled stitching, embroidery, screen printing, and final carton packing entirely within our Sialkot facility.
Quality control operates as a continuous checkpoint system rather than a retroactive check. Every production lot undergoes a four-tier inspection: raw material incoming review, initial pattern piece inspection, mid-line sewing checks, and final random sampling according to ANSI/ASQ Z1.4 (ISO 2859-1) parameters.
Whether you supply engineering tech packs with precise grading rules or request complete sample recreation from benchmark garments, our dedicated R&D department delivers. We provide custom care labels, woven neck bands, custom-molded silicone badges, barcoded hangtags, and Amazon FBA-compliant polybags.
Speed to market defines commercial victory in competitive sportswear seasons. Our dedicated sample development wing operates independently from bulk lines, ensuring rapid counter-sample and pre-production (PP) sample prototyping within 7 to 12 working days with full digital proofing.
Exporting across North America, the European Union, the United Kingdom, Australia, and GCC nations. We execute flexible freight operations under EXW, FOB Karachi, CIF, and door-to-door DDP arrangements via reliable air and ocean courier lines (DHL, FedEx, Maersk, MSC) with full customs clearing paperwork.
We treat club crests, innovative textile coatings, custom design vectors, and branded proprietary grading specifications under strict legal non-disclosure agreements. Your designs are strictly proprietary and never displayed, shared, or repurposed in unauthorized supply pipelines.
Direct technical and operational answers to address common challenges faced by professional athletic directors, brand buyers, and procurement specialists.
Our baseline MOQ is engineered for flexibility. For full-dye sublimation soccer, basketball, rugby, and track uniforms, our production starts as low as 25 to 50 sets per style with unlimited team numbering and individual player name customizations. For complex cut-and-sew articles requiring custom vat-dyed fabric mills or specialized bonded softshells, MOQs typically range from 100 to 300 pieces per colorway.
We provide full technical documentation dossiers (TDF) containing third-party accredited laboratory test reports (SGS, Intertek, or TÜV Rheinland). Reports certify that all base textiles, reflective accents, and chemical printing binders adhere to EU PPE standards (EN 17353, EN 343) and REACH Annex XVII restrictions for heavy metals, phthalates, and banned aromatic amine azo colorants.
The workflow proceeds in 5 disciplined phases: 1) CAD Spec Review & Quotation (24–48 hours); 2) Fabric Lab Dips & Physical Counter-Sampling (7–12 days); 3) Pre-Production (PP) Sample Sign-off; 4) Industrial Mass Production, Automated Cutting & Stitching (3–5 weeks); and 5) Independent AQL 2.5 Inspection followed by palletized export shipping via air freight (4–7 transit days) or sea freight (22–35 transit days).
Yes, private label execution is one of our key offerings. We engineer branded woven jacquard labels, ultra-soft high-definition heat transfer neck prints, branded inner neck seam taping, custom debossed zip pullers, swing hangtags with GS1-compatible EAN/UPC barcodes, and customized compostable or matte ziplock polybags.
Our in-house design engineering team can translate physical samples, vector PDFs, or clear reference photographs into complete industrial tech packs. We generate exact grade measurement charts (spanning youth sizes YS–YXL through adult XS–6XL), seam stitch specifications, and digital sublimation placement vectors at no extra development charge for verified bulk programs.
We utilize the X-Rite Datacolor spectrophotometer calibration system matched against standard Pantone Matching System (PMS) swatches. In dye-sublimation, our Italian high-density sublimation inks are profile-calibrated to specific polyester yarn weaves, ensuring that the delta E (ΔE) color variance between separate seasonal reorders remains <1.0, preserving uniform club identity year over year.
Initiate direct communication with our technical apparel merchandising team in Sialkot. Receive comprehensive FOB or DDP costing models, fabric swatch catalogs, and digital 3D sample renders within 24 hours.
Contact Us